The Press Finished on Time. Why Does Finishing Still Own the Delivery Date?
A printed sheet is not a deliverable. Cutting, folding, laminating, die-cutting, gluing, inspection and packing often decide whether the promise survives.
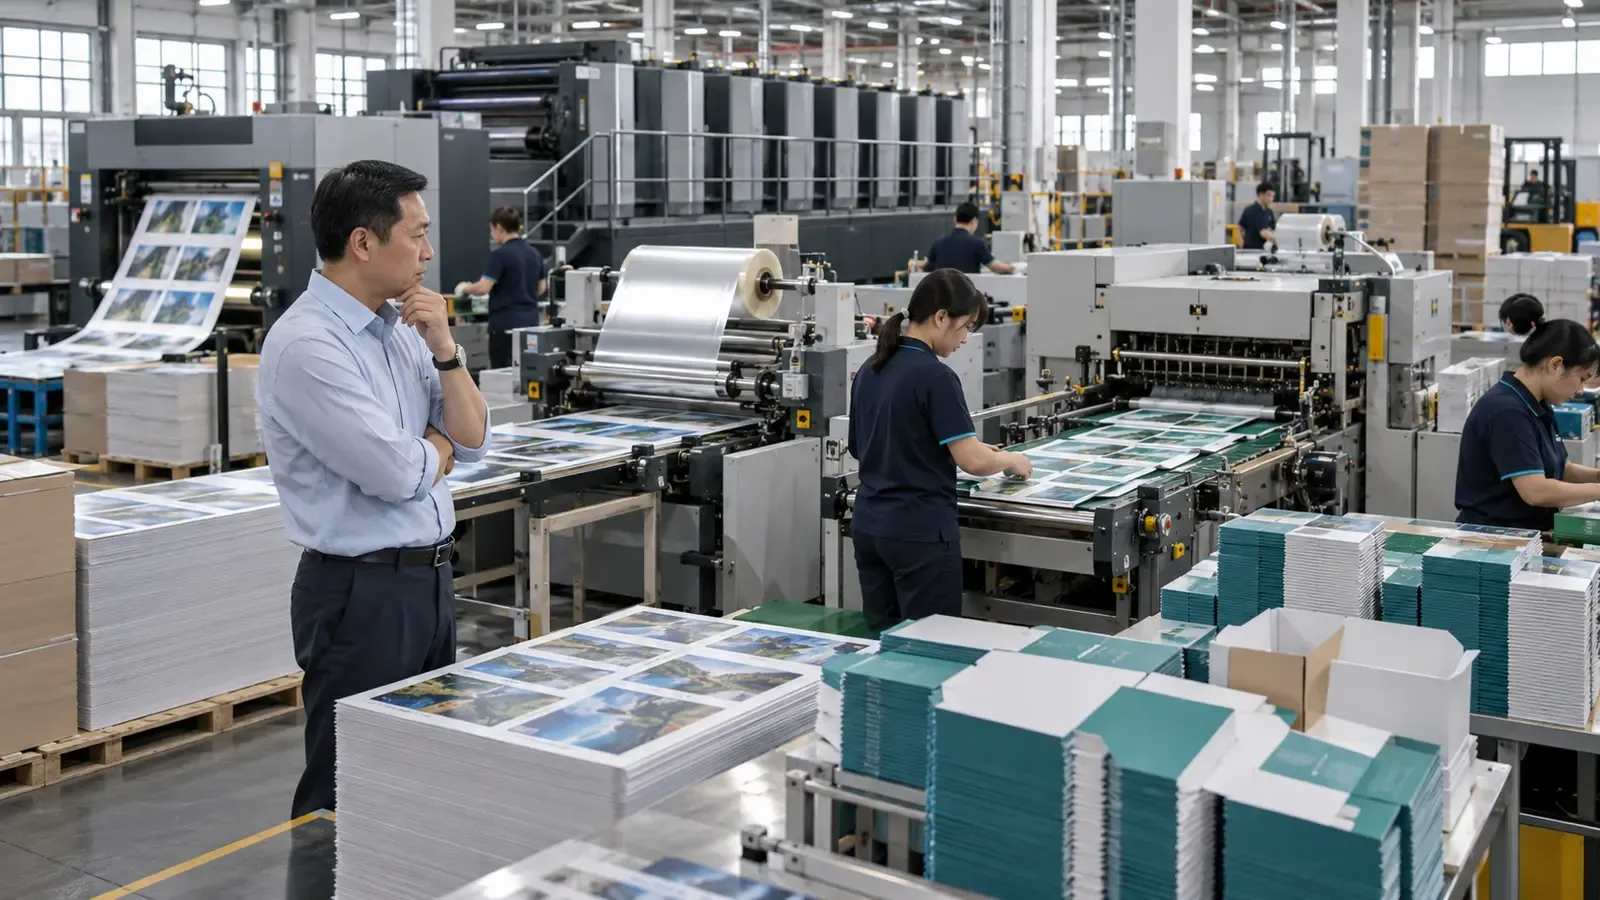
At 6:00 p.m., the press manager reports success. The job is complete, the colour is accepted and the sheets are stacked neatly beside the machine.
Forty metres away, finishing sees a different picture. The laminate has not arrived. The die-cut queue contains two urgent jobs. The glue line needs a change part. The cartons must still be inspected, counted, packed and split across two deliveries.
Printing finished on time. The customer order did not.
The short answer
Print finishing production planning must treat every post-press operation as part of the customer delivery route. Schedule backwards from packed quantity through curing, lamination, cutting, folding, die-cutting, gluing, inspection and outside processing. Track accepted quantities and constraints at each stage. Press completion is a milestone, not the finish line.
The final promise belongs to the whole route, especially its least flexible operation.
The press creates input, not delivery
A freshly printed sheet may still be days from saleable form. Some processes require drying or curing. Others need tooling, specialist skills or batch setup. Defects that are invisible on a flat sheet can appear during folding, creasing or gluing.
If the master schedule ends at the press, finishing becomes an informal recovery department. Supervisors sequence work from physical piles and urgent calls rather than a shared order plan.
Extend the job route to packed and released goods. Every operation should have a planned input time, expected duration, quantity and acceptance point.
Model the real route
“Finishing” is not one operation. A packaging job may travel through coating, lamination, curing, foil, embossing, die-cutting, stripping, window patching, folding, gluing, inspection and packing. Commercial print may need cutting, folding, gathering, binding and mailing preparation.
Record the sequence and dependencies. Lamination may need cure time before die-cutting. A folded section may need correct pagination before binding. A die must be available before the planned slot.
Routes should reflect product families but remain editable for the actual job. An assumed standard route that omits one special finish produces false capacity.
Plan backwards from packed quantity
Start with the delivery time and required good quantity. Work backwards through packing, inspection and each finishing process, adding required transfer or cure time.
This reveals the latest safe completion at the press. A press date can look comfortable until a constrained die-cutter or gluer is considered.
For split deliveries, plan each release lot explicitly. Do not mark the whole job complete because the first portion shipped.
Capacity is product-specific
A finishing machine may be available but unsuitable for the size, material, tooling or quality requirement. Running speed also varies by complexity and substrate.
Use realistic capability:
- compatible dimensions and material;
- required die or change parts;
- setup and wash-up time;
- proven output range;
- operator availability;
- maintenance condition;
- quality risk for the product.
This prevents a nominal open slot from becoming a late discovery.
Watch the queue before it becomes urgent
Finishing queues build because presses release in large batches, priorities change, tools arrive late or one process serves several upstream machines.
Measure ageing and expected arrival, not only current load. A die-cutter that looks free now may receive three press batches together tomorrow.
Use a short horizon showing committed work, likely releases, tool readiness and delivery consequence. Update it with actual press progress rather than waiting for complete pallets to appear.
Transfer accepted quantities
One thousand printed sheets are not necessarily one thousand acceptable inputs to finishing. Spoilage, sampling and quality hold reduce the available quantity.
At each transfer, record:
1. quantity sent;
2. quantity received;
3. accepted quantity;
4. rejected or held quantity;
5. balance outstanding;
6. next-stage release quantity.
This exposes shortages early. The press can decide whether a top-up run is needed before plates and setup disappear.
Quality changes after the sheet changes shape
Colour may be excellent while crease cracking, foil registration, glue strength or folding accuracy fails. Define process-specific first-off approval and in-process checks.
The first converted piece should be assessed while upstream recovery remains possible. If a material or printed feature behaves badly, the team needs a clear containment boundary and decision owner.
Final inspection should confirm the route worked, not discover that an entire batch cannot assemble correctly.
Outside finishing is still inside the promise
Special coatings, foil, binding or conversion may leave the factory. A purchase order and due date do not provide enough control.
Confirm dispatched and received quantities, active specification, tooling, first-off result, progress milestone and return plan. Reconcile the returned balance before closing the external operation.
The customer experiences one supplier. Internal and subcontracted routes must therefore appear in the same delivery view.
Release smaller batches deliberately
Partial transfer from press to finishing can shorten lead time and expose problems earlier. It can also create mix-ups or inefficient repeated setups.
Define minimum transfer quantity, identification, acceptance status and destination. Make sure the next process can actually pull the batch. Moving pallets merely to clear press space shifts inventory without improving flow.
Lean thinking emphasizes flow from the customer’s perspective. The useful question is whether the order moved closer to accepted delivery, not whether one department emptied its floor.
Connect the schedule through one job
An integrated platform such as Jupiter ERP supports production planning and shop-floor visibility across presses and finishing lines. The operating model should connect actual completion and accepted quantity at one stage to the forecast at the next.
When a press runs late, downstream slots should show the consequence. When finishing recovers, shipment should update. Separate department spreadsheets cannot easily maintain this chain.
Measure end-to-end performance
Press utilization and speed matter, but local performance can conflict with delivery flow. Add measures such as:
- press-complete to packed lead time;
- queue time before constrained finishing operations;
- first-off acceptance time;
- finishing spoilage by operation;
- top-up press runs caused by downstream loss;
- plan versus actual packed quantity;
- orders shipped through exceptional recovery.
These measures reveal whether upstream efficiency becomes downstream congestion.
Hold a route-readiness check
Before the press starts, confirm that downstream conditions are credible: tooling exists, outside capacity is confirmed, special material is available and constrained slots are reserved.
This does not require every finishing machine to sit idle waiting. It requires evidence that the complete route can support the promised sequence.
If readiness fails, management can change the press order, expedite a tool, reserve an alternative or revise delivery before ink is on paper.
Create a constraint calendar
Not every finishing asset needs the same planning detail. Identify the operations whose capacity, tooling or skill most often determines delivery and maintain a visible short-term calendar for them.
Include confirmed work, likely arrivals, setup families, maintenance and external commitments. A job entering press should be checked against this future load. When several batches are likely to arrive together, management can sequence, split or secure alternatives before the queue becomes physical.
The calendar should use evidence ranges where press completion is uncertain. False precision creates the same surprise in a more attractive format.
Close the route with packing evidence
Packing is often treated as an administrative tail. In reality, count, version segregation, labels, cartons, pallets and delivery documents can block release.
Define packed and shipment-ready quantities separately. Confirm that packaging materials and instructions match the delivery plan, particularly for split destinations. The last operation deserves the same version and quantity control as the first.
Frequently asked questions
Should finishing control the master schedule?
The master schedule should integrate the whole route. Finishing constraints may determine priorities, but no department should plan in isolation.
Is press completion still an important KPI?
Yes, as one milestone. Pair it with accepted finishing and packed-quantity outcomes so local completion does not hide customer risk.
When should partial batches move downstream?
When identity, accepted quantity and destination are clear, and the next process has capacity to act. Avoid transfers that only create another queue.
How can a factory plan variable finishing speeds?
Use ranges or standards by product and material family, then update them with actual evidence. Highlight new or high-risk combinations.
Finish the customer job
The press deserves attention because it transforms blank substrate into visible value. Yet the customer buys the finished carton, label, book or printed product—not the stack beside the press.
Within the shape-shifting print job, finishing is where flat promises become physical form. Plan it as part of delivery, make its constraints visible and let “complete” mean something the customer can receive.