

The Machine Was Available Until the Style Arrived
An equipment list proves ownership, not readiness. Garment production loses time when maintenance, setup, attachments and technicians meet the style too late.
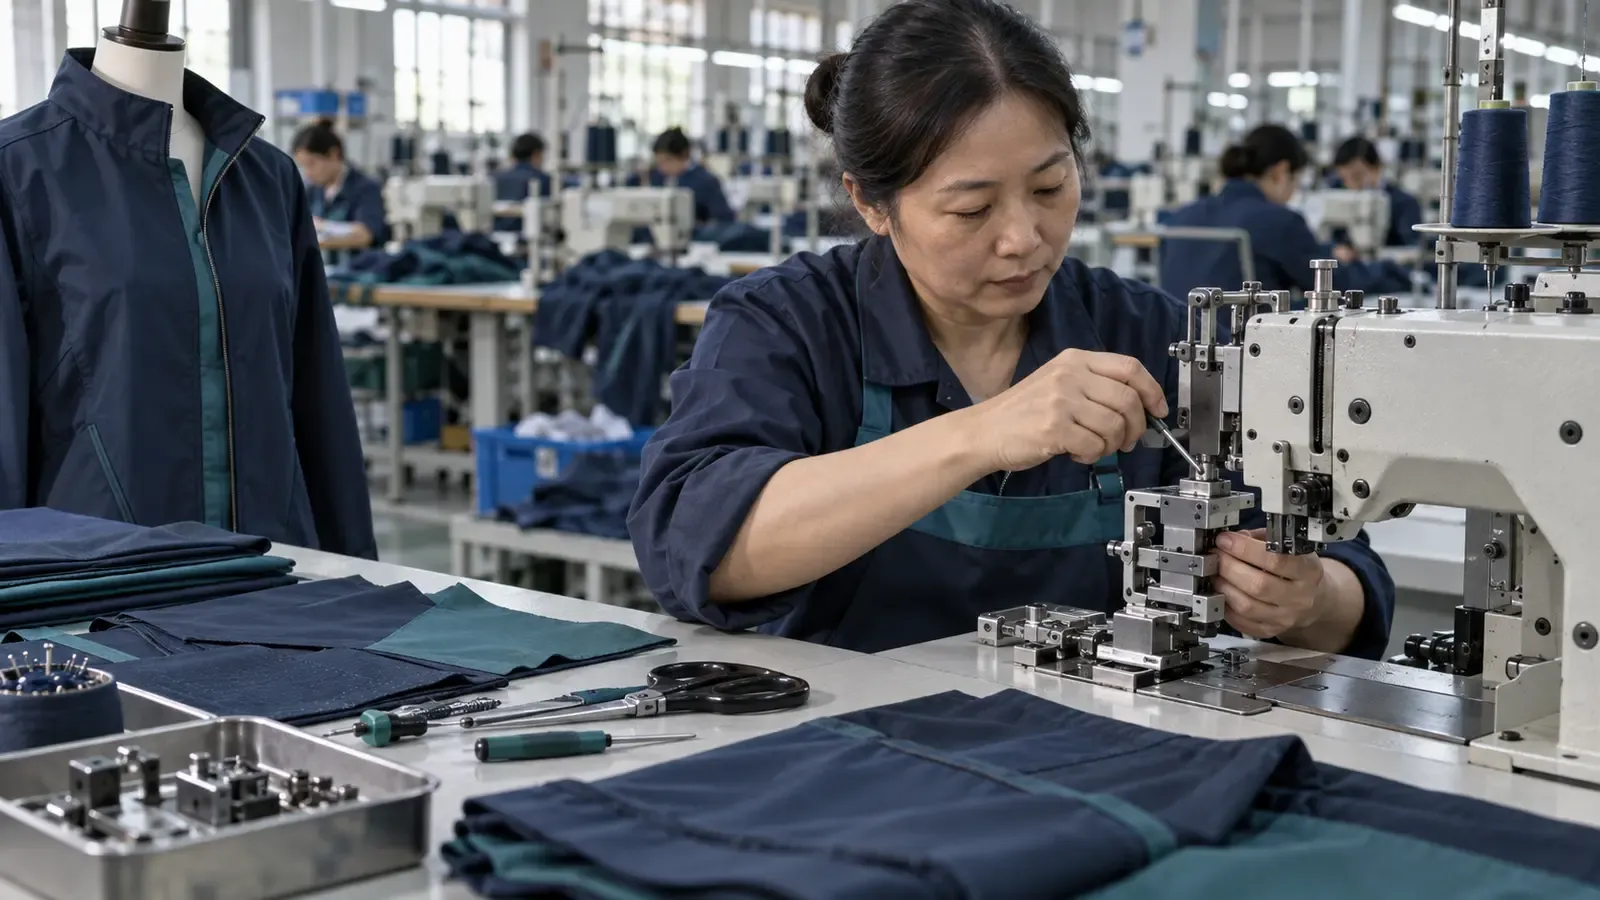
At eight in the morning, the production plan shows an available line. Operators are present. Machines are powered. The new style is scheduled to start.
Then the actual garment reaches the floor.
One operation needs a folder that is still in the tool room. Another needs a feed type that was not listed in the planning meeting. The button machine can run the sample, but not at the required rate. A technician begins adjusting while operators wait, supervisors rearrange work and the schedule quietly becomes fiction.
The machines were available in a calendar sense. The line was not ready in a production sense.
The short answer
Machine availability should be confirmed against the requirements of the specific style, operation and output plan—not inferred from an empty time slot. Readiness includes the correct machine class, attachments, settings, maintenance condition, operator capability, approved method and spare response. These facts should be checked before the planned start, with unresolved gaps visible as constraints.
Capacity is not a count of idle machines. It is the ability to perform the required work at the required quality and rate.
A machine name is not a capability
Planning data may say “lockstitch,” “overlock” or “buttonhole.” Those categories are useful but incomplete. Two machines in the same category can differ in bed type, feed, gauge, attachment, automation, condition and achievable quality on a particular material.
The style introduces its own demands: seam construction, fabric behaviour, thread, tolerances, handling difficulty and target cycle. The intersection of machine condition and style requirement determines readiness.
A capability record should therefore go beyond asset identity. It can include:
- machine class and configuration;
- available folders, guides, gauges and work aids;
- suitable materials and operation history;
- maintenance state and recurring limitations;
- operators currently qualified to run it;
- realistic speed or cycle assumptions by operation type.
The goal is not a perfect engineering database. It is fewer surprises at line start.
Readiness has a deadline before production
If machine preparation begins when operators are waiting, the problem is already late. Define a readiness gate ahead of the start—perhaps during pre-production preparation or a set number of shifts before loading.
At that gate, the team confirms:
1. operation breakdown and method are approved;
2. required machine types and attachments are identified;
3. named assets are available and serviceable;
4. settings or trials are completed where risk is high;
5. operators and technicians understand the method;
6. unresolved gaps have owners and recovery times.
A “not ready” result is valuable when it arrives early. It allows the planner to sequence another style, expedite a tool, arrange training or revise the line design without wasting a full crew’s time.
The sample room knows more than the asset list
The sample room often discovers the practical difficulty first. A pattern shape is awkward to handle. A seam twists. A folder cannot follow the curve. A decorative operation takes longer than estimated. Yet this knowledge may stay with the technician who solved the sample.
Before bulk production, capture the method that actually worked. Which machine and attachment were used? What setting or handling technique mattered? Was the sample made slowly with exceptional skill? Can the proposed production operator repeat it at volume?
The approved sample proves that one garment could be made. It does not prove that the planned line can reproduce it predictably.
Maintenance status must be operational
A maintenance system may label a machine “available” because no work order is open. The supervisor may know that it skips stitches after warming up or that the folder mount loosens at speed.
Readiness benefits from two forms of truth: formal maintenance condition and recent production behaviour. Recurring minor stops, quality defects, speed loss and operator complaints can reveal a machine that is technically running but unsuitable for a critical operation.
Prioritize condition checks for bottleneck and specialist machines. A failure on a common lockstitch operation may be recoverable by substitution. A failure on the only suitable specialist machine can stop the entire style.
Attachments are small assets with large consequences
Factories track major machines carefully but treat folders, guides, gauges and templates as accessories. For many operations, these small items determine both rate and consistency.
Manage them as part of the capability. Give critical attachments an identity, location, compatible machine reference and readiness status. Confirm that the correct version—not merely a similar-looking tool—is at the line.
This also helps after a style finishes. A proven setup can be preserved for repeat orders instead of rediscovered through trial and error.
Operator readiness belongs in the same conversation
A machine can be perfectly prepared while the assigned operator has never used the attachment or construction. Conversely, a highly skilled operator may compensate for poor equipment in a way that makes the plan look feasible but fragile.
Readiness should combine person, method and asset. Ask whether sufficient trained coverage exists for the planned shift, including breaks, absence and rotation. Training should use the actual style method early enough to expose difficulty.
This is not about grading individuals publicly. It is about avoiding a plan that depends on one expert being present every minute.
Build a constraint list, not a green status
One green “machine ready” field hides nuance. A constraint list makes action possible.
For each unresolved item, record:
- exact requirement;
- affected operation and planned start;
- available alternative;
- owner;
- resolution time;
- effect on output if unresolved.
For example: “6 mm folder for operation 24 arrives at 14:00; temporary manual method reduces projected hourly output by 18 pieces.” The precise number should come from local evidence, not optimism. Even without a numeric estimate, naming the affected operation and alternative is better than “tool pending.”
An apparel system such as Venus ERP can connect style, operation and production records so readiness is evaluated in the order context. The discipline lies in keeping those records current and using them before the line is loaded.
The first hour is a test of the preparation system
Measure line start as a distinct event. How long from planned start to the first accepted piece? How many stops were caused by method, machine, attachment, material or training gaps? When did stable output begin?
These facts turn every start into feedback. If the same readiness gap repeats, improve the pre-start gate rather than celebrating another recovery.
Useful start metrics include:
- planned versus actual first accepted piece;
- minutes lost by readiness category;
- operations changed after loading;
- tools borrowed or substituted;
- time to stable quality and flow;
- repeat issues from earlier styles.
The measure should not encourage teams to declare a premature start. A style has started when it can produce accepted work, not when the first operator touches a panel.
Protect the schedule from false availability
Planning systems need a way to distinguish reserved, available, conditionally ready and blocked capability. A specialist machine promised to two lines is not truly available. A machine awaiting an attachment is conditional. A machine under trial is not equivalent to proven capacity.
This richer status helps planners decide with evidence rather than learning through floor disruption. It also exposes whether the factory routinely solves readiness after the planned start—one of the recurring causes of the waiting factory.
Frequently asked questions
How early should machine readiness be checked?
Early enough to resolve the longest likely gap. Common setups may need a short lead; specialist tools, parts or training may need days. Set the gate from risk, not habit.
Should every machine have a detailed capability profile?
Start with specialist, bottleneck and high-risk equipment. Expand where the profile prevents recurring planning errors. Avoid collecting fields that no decision uses.
Is preventive maintenance enough to prove readiness?
No. Preventive maintenance supports condition, but style readiness also depends on configuration, tooling, method, material and operator capability.
What if an alternative manual method exists?
Record it with its quality and output implications. An alternative can support a conscious recovery plan, but it should not silently preserve an unrealistic original target.
Make readiness real before the shift begins
The strongest line start is almost uneventful. The right machines are present, the attachments fit, the approved method is understood and the first piece confirms what preparation already predicted.
That calm is not luck. It is the result of treating availability as a style-specific capability decision—and making that decision while there is still time to act.