

One SKU, Three Language Versions. How Do You Prevent Version Mix-Ups on the Shop Floor?
Version errors often happen when similar jobs share artwork families, common materials or neighbouring machine time. Prevention depends on disciplined release, physical separation, clear identification and controlled packing logic.
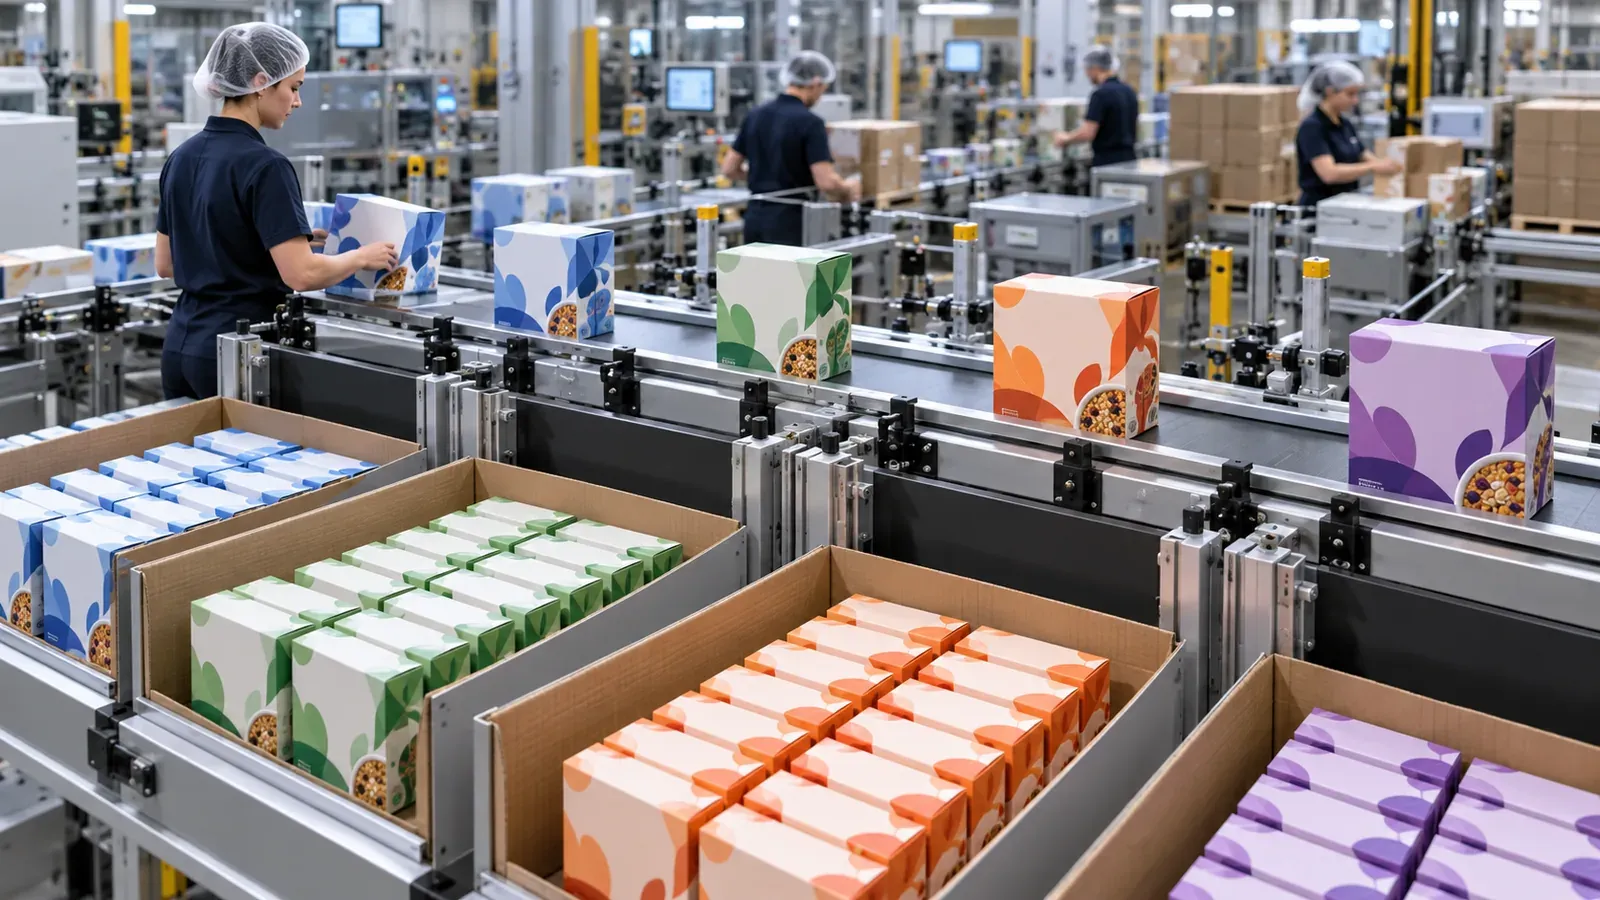
Version errors often happen when similar jobs share artwork families, common materials or neighbouring machine time. Prevention depends on disciplined release, physical separation, clear identification and controlled packing logic.
Why this matters
This article examines one operational branch of How Do Change and Version Decisions Create Hidden Risk in Printing and Packaging? and explains how to control packaging version mix-up prevention in a practical print-and-packaging workflow.
Version mix-ups are usually system failures, not operator failures
When one SKU has multiple language or customer versions, the risk is not simply that someone becomes careless. The real issue is whether the production system makes the correct choice clear and the incorrect choice hard. Similar artwork families, shared substrates and adjacent machine time all increase confusion unless there is deliberate separation. Operators should not have to rely on visual memory when many variants look similar from a few metres away.
Release packets must identify the version unambiguously
Every floor packet should make the current version identity obvious. That means using one version reference across the proof, work order, pallets, bin labels, print samples and packing instructions. When one document says “Spanish,” another says “LATAM,” and a third uses a revision code only customer service understands, confusion becomes likely. Operationally, the best release packet minimises translation work on the floor.
Physical segregation matters as much as digital control
Digital version control is essential but it does not replace physical discipline. If different language versions are staged in neighbouring bins, printed in overlapping windows or packed into the same area, an otherwise good digital system can still fail. Separate lanes, distinct tote or pallet identities and clear hold boundaries reduce opportunity for mix-up. Physical controls are especially important at shift changes and during rework, when teams re-enter a job midstream.
Packing logic is often the last weak point
A job can survive prepress and press without error and still fail during packing. Similar cartons may be picked into the wrong case, mixed onto one pallet or loaded against the wrong label. Where multiple versions share the same day, management should verify case labels, pallet identities and loading sequence as carefully as it verifies the press run. The loading dock is not too late for version control; it is part of it.
This is one branch of the pillar challenge
Preventing variant confusion is one operational branch of change control and version management in printing and packaging. The pillar issue is bigger than line segregation alone, but the shop floor reveals whether upstream version control is strong enough to survive real production pressure.
Use visual differences only as a support, not the control itself
Colour-coding or accent graphics can help separate versions, but they should support rather than replace formal identification. Visual distinctions fail when artwork families are intentionally similar or when products are viewed at distance. The core control is still the version-linked release packet and disciplined material flow.
Audit the handoff points where mix-ups begin
Most version errors begin at handoffs: prepress to press, press to finishing, finishing to packing or packing to dispatch. Short floor audits at those interfaces are more useful than large end-of-month reviews because they show where identification becomes ambiguous. The purpose is to harden the handoff, not to assign blame later.
Design the exception path as carefully as the normal path
Rush changes, line restarts, partial rework and leftover inventory are the moments when mixed versions are most likely. Plants should decide in advance how suspect material is held, how partially packed cases are relabelled and who can re-release interrupted work. The exception path deserves the same clarity as normal production.
Management checklist
- Confirm the current version identity before action.
- Check which downstream assumptions depended on the previous state.
- Separate obsolete or suspect material physically.
- Assign a clear release or escalation owner.
- Record the impact so the next job benefits from the evidence.
What management should measure
For packaging version mix-up prevention, track how often the issue appears, what quantities are placed on hold, the extra setup or proofing time created, and whether the same cause recurs on later jobs. Trend these measures by customer family and process stage so that management can distinguish one-off exceptions from structural weakness. The purpose is not to punish variation; it is to learn where release and version discipline should become stronger.
Frequently asked questions
Is every approved customer change a full restart?
No. The correct response depends on what changed. Some revisions require only a limited revalidation, while others can invalidate tooling, materials or route assumptions and therefore need a much deeper review.
Why are repeat orders still risky?
Because repeat work encourages assumptions. A prior successful run is useful evidence, but it does not prove that the current order still has the same version, material, process and release requirements.
What is the difference between approval and release?
Approval confirms what the customer accepted. Release confirms that the plant has the correct operational combination to execute that accepted version safely and correctly.
Why is shipment proof part of change control?
Because the final question is whether the correct approved version and material actually reached the customer. If that cannot be proven, the change-control chain is incomplete.
Similar-looking leftovers are a major risk source
Leftover printed sheets, partially filled cases and unconsumed labels can quietly undermine otherwise strong controls. If the plant stores these items without clear status and identity, they become attractive shortcuts on a future shift. A disciplined disposition process for leftovers is therefore a direct mix-up prevention tool.
Training should focus on decision moments, not only procedures
Operators usually understand the idea of version control in principle. The real value of training is to show what to do at the moments of uncertainty: when two versions are staged nearby, when one bin runs short, when a label is missing, or when a restart occurs after interruption. Training that rehearses these moments improves practical control far more than generic awareness sessions alone.
Short verification loops reduce dependence on memory
A second-person check at the right moment can be extremely effective, especially at release to packing and release to dispatch. The most useful verification loops are short and targeted. They confirm the critical identity of version and destination without slowing the whole line down.
Customer complaints should be translated into control improvements
When a version complaint occurs, the plant should map it back to the control point that failed: release packet clarity, physical segregation, label identity, packing sequence or dispatch handling. This avoids generic corrective actions and strengthens the specific place where confusion entered the flow.
Supervisor checks should concentrate on mixed-version windows
Not every production hour has the same mix-up risk. The highest-risk windows are setup, restart, shift change, rework and packing transition. Brief supervisor attention in those windows gives far more control value than broad low-intensity monitoring all day.
Segregation standards should extend to digital picks and labels
As more lines rely on scanners, digital picks and printed labels, segregation must include those digital selection points as well as physical bins. The right on-screen choice and the right printed identity should reinforce one another so that the floor is not depending on only one mode of control.
Schedule sequencing can reduce the opportunity for confusion
Version control is easier when production planning considers the risk of running near-identical variants back to back. Where practical, planners can sequence jobs to create cleaner separation between versions or ensure that one version is fully cleared from the line before the next enters packing. This does not mean sacrificing efficiency unnecessarily. It means recognising that the cheapest schedule on paper can become expensive if it increases the probability of mixed WIP, labels or cases.
Clear-down standards should cover every reusable item
At the end of a version run, the line should clear not only finished cartons but also loose labels, retained samples, setup sheets, partially used bundles and temporary identification cards. Small reusable items are common carriers of version error because they survive after the main WIP is removed. A defined clear-down check protects the next run and gives supervisors confidence that the area is genuinely reset rather than merely looking tidy.
Treat partial quantities as separate control events
When a version run is split across shifts, machines or delivery dates, the remaining quantity should not be treated as an informal continuation. Reconfirm the version identity and the remaining WIP before restart so that leftovers from another variant cannot enter the balance quantity. This small restart discipline is particularly valuable when similar packs share the same substrate and finishing route.