The First Good Sheet Arrived Late—and Took the Job’s Margin With It
Makeready loss is more than setup minutes: plates, colour, substrate, approvals and trial sheets combine before saleable production can begin.
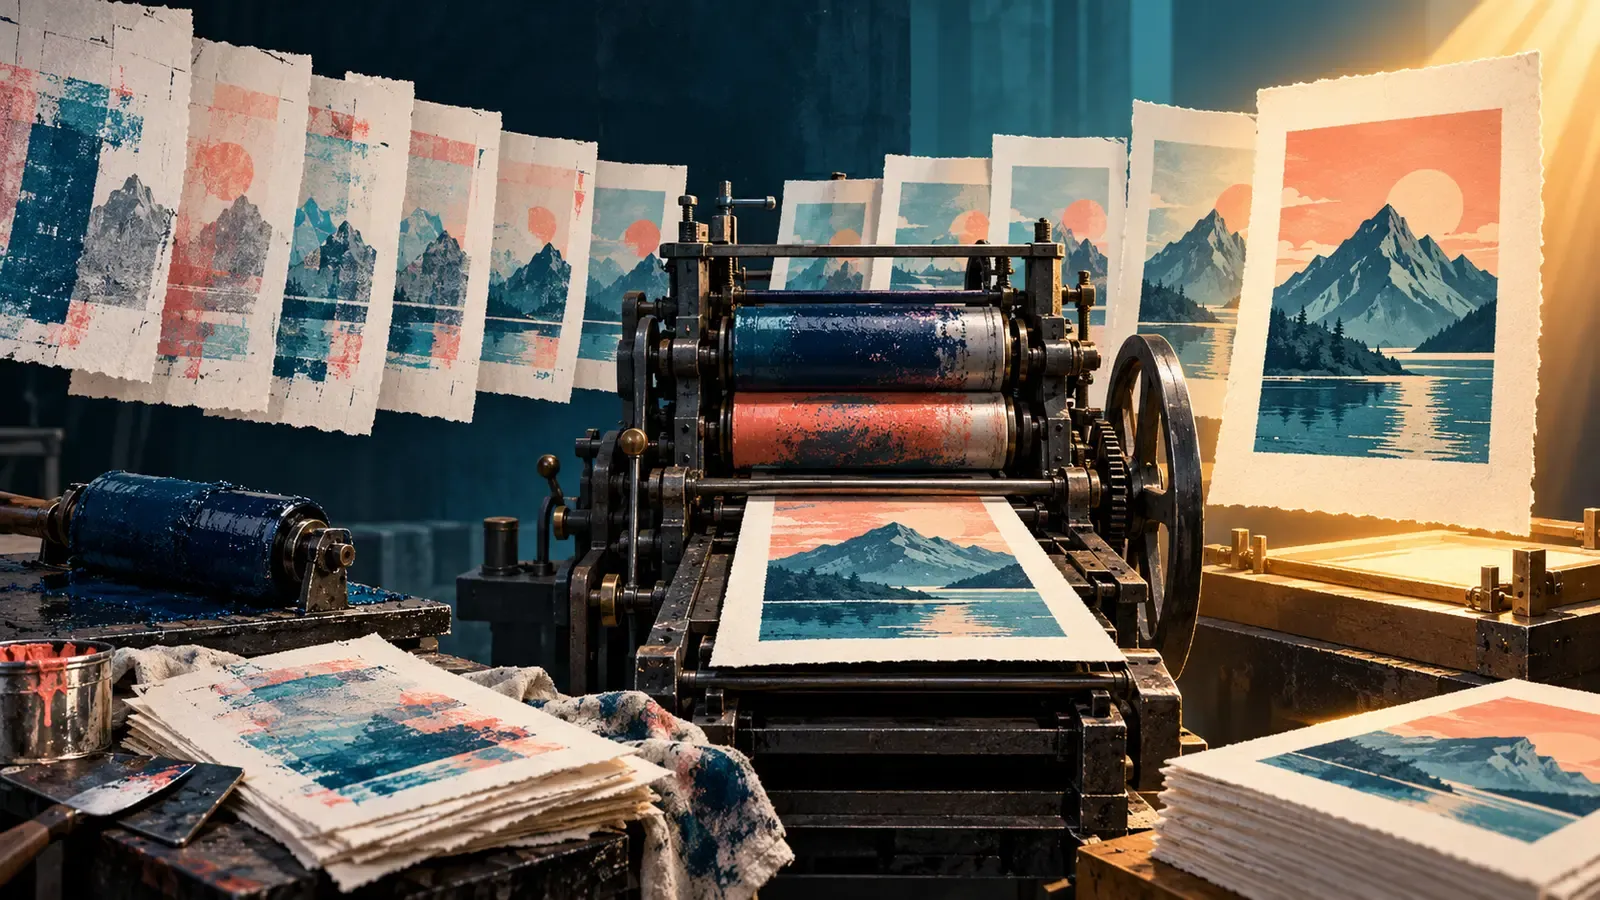
The press starts at 8:00. The first good sheet is signed at 8:47.
Between those times, plates are adjusted, colour is chased, register is corrected, paper is tested and trial sheets gather beside the machine. The schedule records a job start at eight. The customer value starts forty-seven minutes later.
On a short run, those missing minutes and sheets may carry away much of the margin before saleable production begins.
The short answer
Printing press makeready reduction begins by measuring the full interval from the last accepted sheet of the previous job to stable accepted output of the next. Separate preparation that can occur before the press stops from work that requires the machine. Connect time, trial sheets, plate changes, colour adjustment, approval delay and restart quality to job cost.
The aim is not the fastest possible first sheet. It is a predictable first good sheet with stable production behind it.
Define the clock consistently
Factories often compare incompatible makeready figures. One clock begins when plates enter the machine. Another begins after cleaning. A third stops at the first impression, regardless of quality.
Record several milestones:
- last accepted sheet of the outgoing job;
- press available for conversion;
- plates and substrate loaded;
- first impression;
- first accepted sheet;
- stable accepted output.
These timestamps separate cleaning, physical setup, adjustment, approval and stabilization. Improvement becomes specific.
Count trial sheets by reason
A single waste quantity does not explain loss. Categorize trial sheets for register, colour, ink-water balance, plate issue, substrate behaviour, mechanical adjustment, customer approval or another defined reason.
Keep categories practical. The operator should record them without interrupting safe work. Review recurring causes by press, product and material.
If colour adjustment dominates one product family, investigate standards and ink preparation. If plate issues repeat, look upstream. If accepted colour takes long because the approver is absent, the machine problem is actually a decision problem.
Move preparation off the stopped press
Before the current job ends, teams can often prepare:
- verified plates and active artwork revision;
- correct paper, board or reel;
- ink and colour target;
- blankets, tools and cleaning materials;
- job ticket and quality criteria;
- operator and approval availability;
- next-job logistics near the machine.
Only work that truly needs the stopped press should remain inside the changeover interval. Searching and clarification are preparation debt.
Close the outgoing job properly
Rushing the next setup can create unresolved balance on the previous job. Confirm final accepted quantity, residual paper, ink handling, plate status, quality hold and any planned top-up.
Without closure, teams may later remount plates for a small shortage or discover mixed material. That second setup is part of the original failure even if recorded under another day.
Verify the active revision before mounting
A fast setup with the wrong plate is the most expensive kind of speed. Match job, artwork revision, plate identity, version quantity and proof before production use.
The controls described in artwork version control should make verification simple. If operators must search messages or compare visual details under pressure, upstream release is weak.
Obsolete plates should be physically separated and systemically unavailable for selection.
Colour approval is a planned resource
The press can reach a technically stable condition and still wait for authorization. Decide who can approve, what target applies and who acts as backup.
Provide the approved proof, spectral or density target, substrate context and tolerance required by the business. If customer attendance is necessary, schedule the decision window with the same seriousness as machine time.
Track approval waiting separately from adjustment. That distinction shows whether the team needs better process control or better decision readiness.
Standardize by job family
One universal makeready standard hides meaningful differences. A repeat label on familiar stock is not equivalent to a new high-coverage carton with special coating.
Group jobs by drivers such as press, colour count, substrate, plate type, complexity and repeat status. Establish expected ranges from actual evidence.
Use the range to plan and to detect abnormal performance—not to pressure operators into accepting a poor first sheet.
Sequence work to reduce conversion burden
Scheduling can reduce makeready by arranging compatible jobs: similar substrate, colour family, size or coating. But sequencing must still respect delivery and downstream capacity.
A convenient press sequence that overloads finishing does not improve the customer flow. Use the complete route, as explained in why finishing owns the delivery date.
When compatible sequencing is chosen, show the assumed saving in the plan and compare it with actual results.
Connect makeready to margin
Time and sheets consumed before stable output have financial value. Assign actual press time, material and consumables to the job according to the company’s costing method.
Compare estimate and actual. For short runs, fixed setup can dominate unit economics. For long runs, a slow stabilization period may matter more than the first few minutes.
An integrated platform such as Jupiter ERP combines production execution and job-cost visibility. The record should show why loss occurred, not merely that actual cost exceeded estimate.
Protect quality during speed improvement
Makeready programmes can create the wrong incentive if the only target is minutes. Operators may present a marginal sheet for approval or begin production before the process stabilizes.
Use paired measures:
- time to first accepted sheet;
- trial sheets to acceptance;
- time from acceptance to stable output;
- early-run defects or stops;
- repeat adjustment after release.
Faster acceptance with more downstream rework is not improvement.
Learn immediately after the run
Hold a short review while evidence is fresh. What exceeded the expected range? Which item was unavailable? Which adjustment repeated? Which task could have moved offline?
Capture one or two changes with owners. Update setup instructions, material notes, colour target or preparation checklist for the next comparable job.
The learning should return to estimating as well. If a job family consistently requires more sheets or time, the commercial model needs evidence.
Make the loss visible without blaming
Operators are often the people who rescue weak preparation. A fair review separates controllable execution from missing inputs, poor plates, unstable materials and approval delays.
Go to the press and observe the sequence. Lean thinking encourages understanding work where it occurs. Ask which motion, search, wait or repeated adjustment adds no value and what upstream change would remove it.
Improvement is strongest when the crew helps design it.
Separate repeatability from speed
The strongest makeready process produces a narrow, predictable range across comparable jobs. One exceptional fast setup followed by several long ones does not create dependable capacity.
Review variation as well as averages. Identify which inputs were present on the stable runs and missing on the unstable runs. Standard work should capture the preparation sequence, verification and acceptance method that made good performance repeatable.
This gives scheduling a credible expectation and reduces the amount of hidden protection placed around the press plan.
Make improvement visible in the next schedule
When a team removes an external task from stopped-press time or improves a plate check, update the planning standard carefully. Test the new range across enough comparable work before promising all of the saving commercially.
Improvement should create usable capacity, not merely a favourable workshop result. Observe whether downstream finishing and quality remain stable when the press releases work earlier.
That is the test that turns a faster setup into dependable operational capacity.
Frequently asked questions
What is a good makeready time?
There is no universal number. Compare consistent definitions within similar presses and job families, then reduce avoidable variation while protecting quality and safety.
Should wash-up be included?
Include all time from last accepted output to stable accepted output, then separate components. This prevents loss from moving outside the chosen definition.
How should trial sheets be valued?
Use the company’s material and costing rules, linked to actual substrate and job. Physical quantity and reason remain useful even before perfect financial allocation.
Can automation solve makeready loss?
Automation can reduce adjustment and improve repeatability, but wrong revisions, missing materials, weak standards and delayed approvals still require workflow control.
Let the first good sheet tell the truth
Makeready is where the quoted production model meets the press. The interval exposes whether artwork, plates, material, people, standards and decisions were genuinely ready.
Inside the shape-shifting print job, that first accepted sheet is more than a quality milestone. It is the moment the factory begins creating the output it priced—and the moment margin stops waiting beside the machine.