

Printing Finished on Time. Why Is the Job Still Late?
Press completion is only one milestone. Finishing, inspection, packing, consolidation and loading can become the real constraint that determines whether a printing or packaging order ships on time.
The short answer
A job is not complete when the press stops. It is complete when the required finished quantity has passed the remaining operations, quality checks, packing and shipment preparation. Printing on time can therefore coexist with late delivery when the real bottleneck sits in coating, lamination, die-cutting, folding, gluing, binding, inspection, packing or loading.
Press completion is an internal milestone, not the customer outcome
The press is highly visible and often expensive, so plants naturally focus on its schedule. But the customer buys finished cartons, labels, books, displays or other usable products, not printed sheets. If downstream capacity is not planned with the same discipline, the organization can report strong press performance while orders remain stuck in WIP. The schedule should therefore represent the complete route to shipment.
Finishing capacity is often more fragmented than press capacity
A job may pass through several smaller resources after printing, each with different tooling, skills, batch sizes and changeovers. Some work is internal and some outsourced. This fragmentation makes congestion harder to see. A die-cutter can become the constraint for one product family while gluing or inspection constrains another. Planners need capacity by operation and job compatibility rather than one generic finishing queue.
WIP hides lateness until the final days
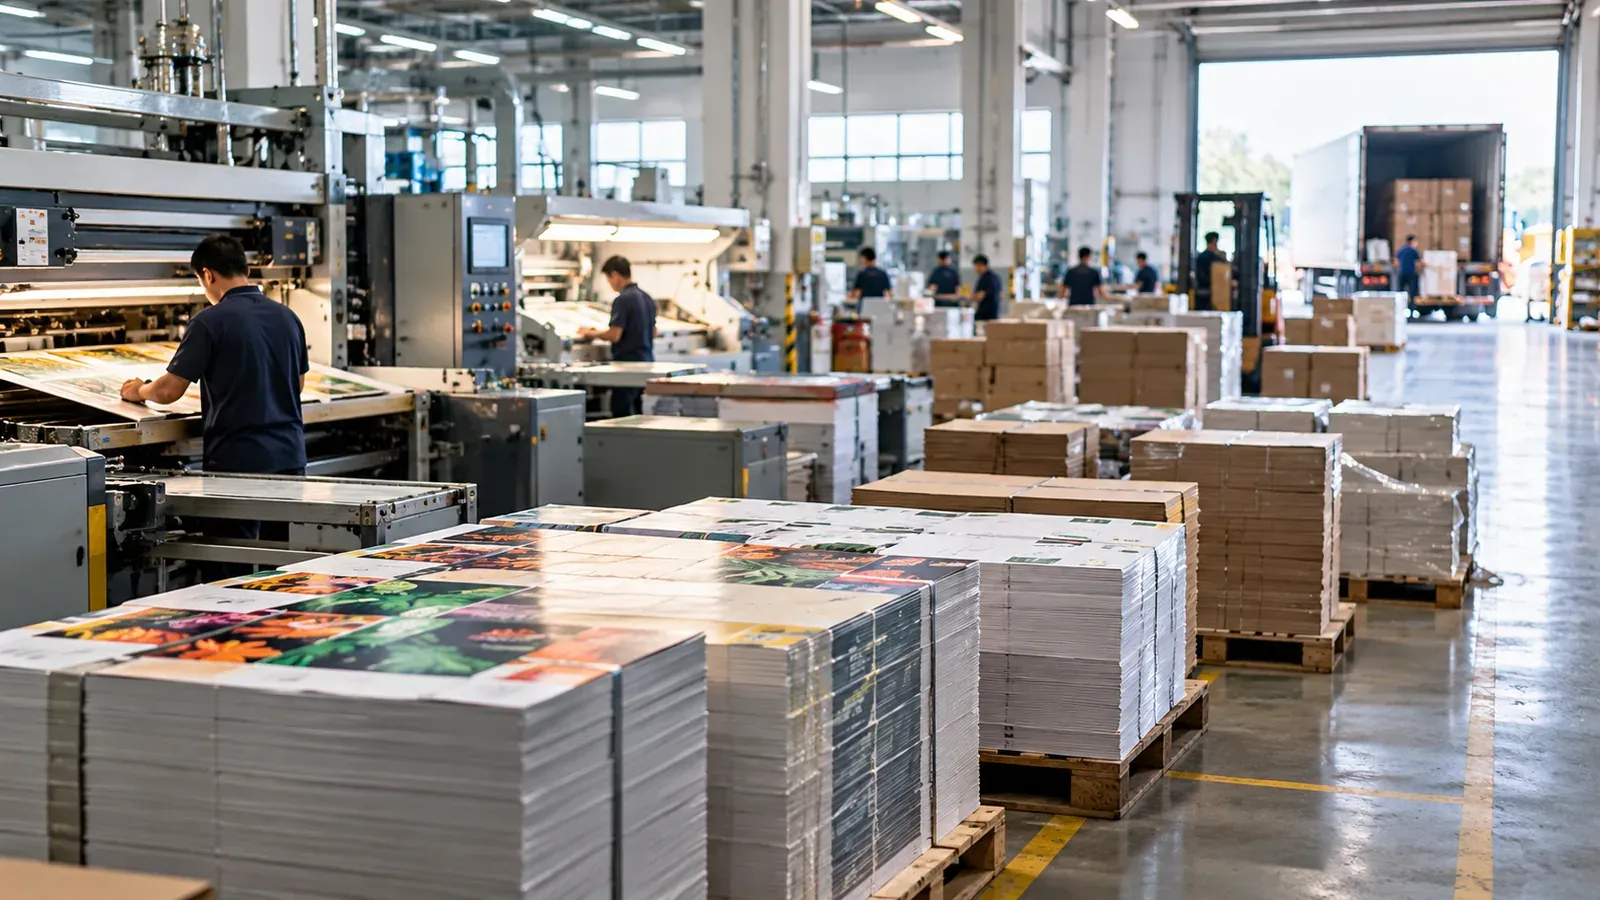
Large piles of printed work can create the impression that production is ahead. In reality, WIP is unfinished demand waiting for the next resource. When many jobs accumulate before finishing, the plant loses flexibility and priority conflicts increase. Measuring queue time between major operations helps reveal the problem earlier than the shipment date.
Quality holds can move the real completion date
Inspection and quality release should be treated as scheduled work, not an administrative step after production. Rework, sampling, colour or structural checks and customer-specific inspection can all add time. If quality resources are overloaded or the job arrives with known issues, the finished quantity may not be available for packing even when manufacturing operations appear complete.
Packing and consolidation deserve capacity planning
Packaging manufacturers can themselves underestimate packing. Different SKUs may need counts, separators, labels, pallets, mixed-order consolidation or export preparation. A job that finishes in several batches can wait for the final component before shipping. Planning the packing and consolidation logic alongside production reduces the last-minute rush at the dock.
Shipment scheduling should use finished-ready quantity
A truck booking based on planned press completion is fragile. Shipment should be connected to the expected completion of the full routing plus inspection and packing. For partial deliveries, the business should know which quantity is truly releasable and whether splitting creates additional freight or administrative cost. This prevents transportation plans from becoming another source of expediting.
Priorities must be consistent across departments
A common failure occurs when the press prioritizes one job, finishing another, and logistics a third. Each department may optimize its own target while the overall order suffers. A shared job priority based on customer commitment, readiness and business impact helps all stages pull the same orders through the system. Exceptions should be visible to the entire flow, not negotiated separately at each machine.
Measure order flow, not only department performance
Useful measures include end-to-end lead time, queue time between operations, WIP age, schedule adherence by finishing process, quality hold duration, packing completion and shipment readiness. Department utilization still matters, but it should not dominate. The management goal is reliable order completion, not maximum local activity.
A practical daily completion review
Review orders due to ship in the next few days and work backward from shipment readiness. Confirm remaining operations, required quantities, finishing capacity, quality status, packing materials and transport booking. Highlight orders whose next required resource is not available in time. This creates a short, action-oriented exception list and prevents printed-but-unfinished work from disappearing into the plant.
How Jupiter supports end-to-end control
ACC — Jupiter Printing & Packaging ERP connects production planning, shop-floor execution, shipment scheduling and job costing across the print workflow. The important management effect is a single view of where the order actually is, so “printed” is not mistaken for “ready to ship.”
Related ACC Insights
- Why Printing and Packaging Jobs Lose Margin Between Quote and Shipment
Management checklist
- Confirm the current job assumption that management is relying on.
- Compare the planned condition with the latest operational evidence.
- Identify whether cost, capacity, quality or delivery commitment has changed.
- Assign an owner and decision time for material exceptions.
- Keep the reason for the decision attached to the job for post-job learning.
Schedule the whole route, not only the press
Printing is often the most visible operation, but it is not necessarily the operation that determines shipment. A carton may still require coating, die-cutting, stripping, folding, gluing, inspection, packing and palletisation. Commercial print may need binding, trimming, collating or external finishing. If those steps are treated as unlimited downstream capacity, the press schedule can release more work than the rest of the factory can absorb.
A route-based schedule assigns a realistic next operation and expected queue for every job. The purpose is not to predict every minute perfectly. It is to prevent the false conclusion that an order is nearly complete simply because its largest machine operation has finished.
Make WIP age visible between operations
Queue length alone does not show urgency. Ten pallets waiting for die-cutting may be normal if they arrived recently; three pallets may be serious if one has already consumed most of its delivery buffer. WIP age therefore gives managers a useful early-warning measure. It shows where completed work is waiting instead of progressing toward shipment.
The same logic applies to quality hold and packing. A finished quantity that is not released, consolidated or packed to customer requirements is still operationally incomplete. Tracking the timestamp at each handoff helps management distinguish productive processing time from waiting time.
Protect the loading promise with a completion definition
Every business needs a clear point at which a job is considered complete. For delivery control, that point should normally mean the required quantity has passed its required operations, is quality released and is physically ready for the intended shipment. Press completion is only an intermediate milestone.
This definition improves escalation. If a job is printed but not shipment-ready, planners can see the exact remaining route and the capacity required. Sales can communicate from an evidence-based status rather than assuming that “printed” means “done.” Operations can also identify whether the recurring constraint sits in die-cutting, gluing, inspection, packing or loading.
The connection to overall profitability is explained in Why Printing and Packaging Jobs Lose Margin Between Quote and Shipment. Downstream queues matter because expediting, overtime, extra handling and missed shipment promises can erode the margin that appeared secure when the press finished.
Balance downstream work before the queue becomes visible
A finishing bottleneck is easier to prevent than to recover from. Before releasing another large press batch, planners should compare expected output with the receiving capacity of the next critical operation. If die-cutting, gluing or packing is already carrying aged WIP, advancing more print may only consume floor space and handling effort. Smaller transfer quantities can sometimes let finishing and inspection begin earlier, but the right rule depends on setup economics, handling risk and due date.
Use shipment cut-off as a backward planning point
For jobs with a fixed collection or export cut-off, planning should work backward from the latest acceptable loading time. That exposes how much buffer remains for inspection, packing, palletisation and documentation after finishing. When the remaining buffer shrinks, the job can be escalated before it becomes a loading emergency. This is more useful than reporting only the percentage of operations completed because the final hours often contain the dependencies that actually determine whether the order leaves on time.
Frequently asked questions
Why can a job be late after printing finishes on time?
Because downstream finishing, inspection, packing, consolidation or loading may still require significant capacity and can become the true bottleneck.
What is the best way to see a finishing bottleneck early?
Track WIP age and queue time by the next required operation. Growing queues before a specific process indicate that downstream capacity is becoming constrained.
Should packing be included in the production schedule?
Yes when packing requires meaningful labour, materials, consolidation or customer-specific handling. Treating it as an afterthought creates avoidable shipment risk.
Which completion date should management use?
Use the date when the required quantity is fully processed, quality released and ready for shipment, not merely the press completion timestamp.