

Plates, Dies and Files Are Ready. How Do You Release Only the Correct Combination to Production?
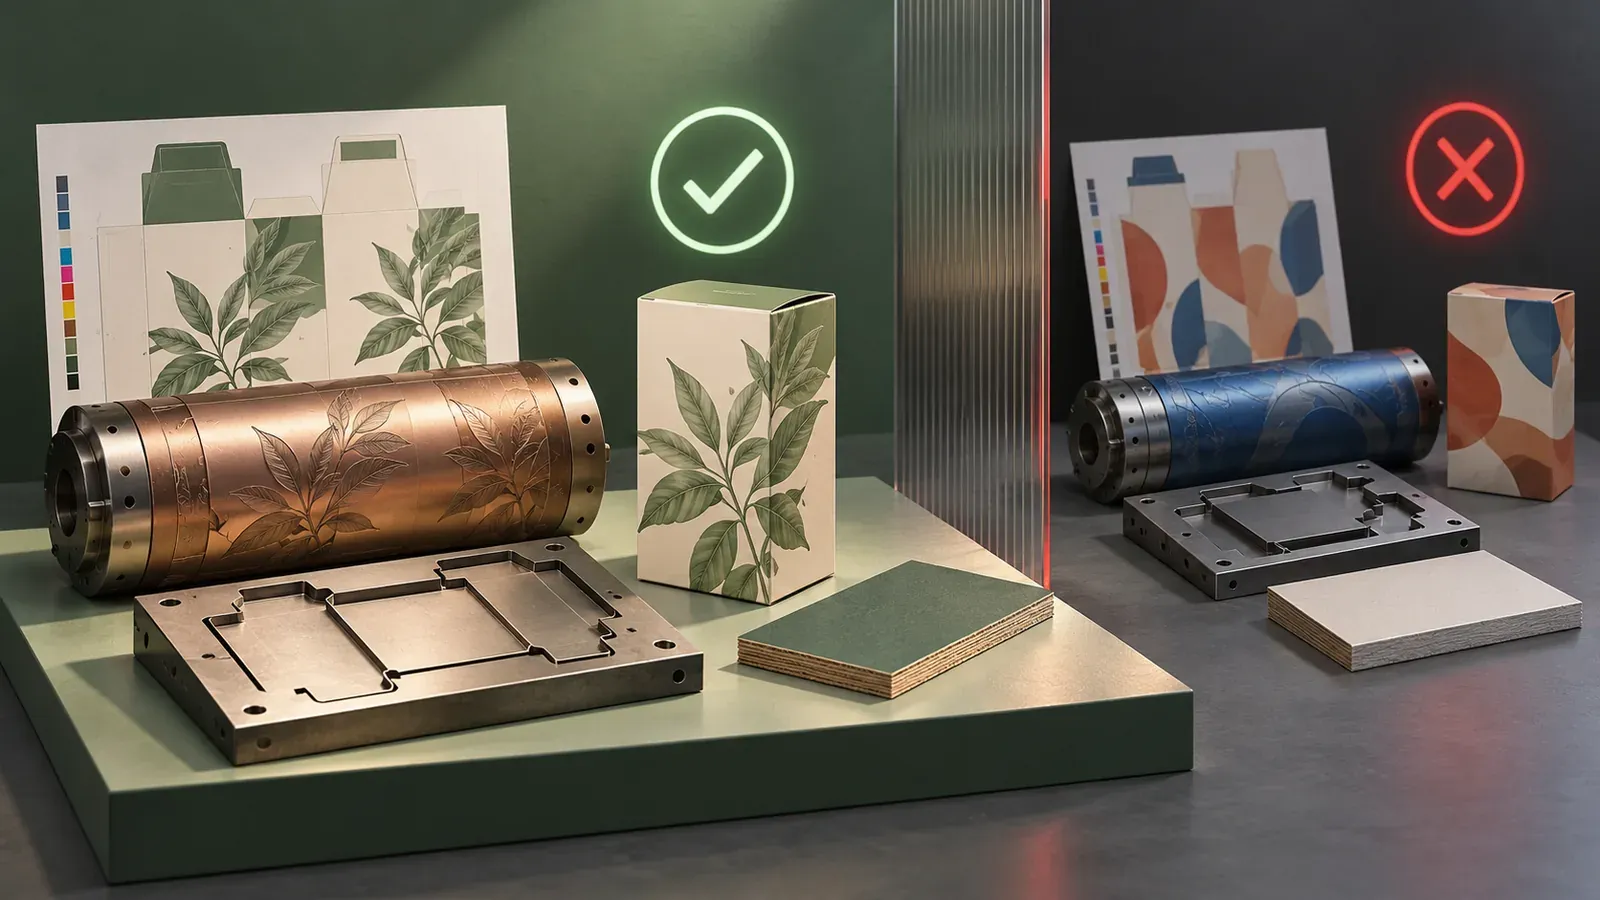
Production readiness is not about checking boxes independently. The release decision must confirm that the approved file, plate, die, substrate and routing belong together for the same version and job context.
Production readiness is not about checking boxes independently. The release decision must confirm that the approved file, plate, die, substrate and routing belong together for the same version and job context.
Why this matters
This article examines one operational branch of How Do Change and Version Decisions Create Hidden Risk in Printing and Packaging? and explains how to control correct file plate die substrate release in a practical print-and-packaging workflow.
Availability is not the same as compatibility
Shops often ask whether the file is approved, whether the die is in stores and whether the board has arrived. These are necessary checks, but they do not answer the most important release question: do the available components belong together for the current version? Production consumes a coherent combination, not a shopping list. Compatibility should therefore sit at the centre of the release decision.
The release gate should compare identities, not only names
Human-friendly item names can be similar across versions, especially on repeat work. A better release gate confirms that the job, version, substrate, tool and route identities match the same released combination. If any one element points to another revision, the release should stop until the mismatch is resolved. This is faster than reworking the consequences after machine time begins.
Approved versus rejected setup should be physically obvious
Where possible, the plant should make the correct combination visually and physically obvious during setup. Keep the released file packet, proof and tool set together. Separate superseded materials clearly. Prevent “almost right” components from sitting alongside released ones. A clean physical setup reduces the chance that operators combine available parts by convenience.
Ownership of release matters
One owner should hold responsibility for final release, even if several functions contribute evidence. Prepress may confirm the file, stores may confirm the board, and tooling may confirm the die, but someone must decide that the production combination is valid. When release ownership is ambiguous, teams tend to assume that another function already checked the full combination.
This release question connects directly back to the pillar
This article explores one control point inside the broader topic of change control and version management in printing and packaging. The pillar issue is whether the current job identity still governs everything released to the floor.
Short release bundles are stronger than long document trails
Operators usually need a concise release bundle: approved proof, current route, current substrate callout, tool identity and clear status. Long document trails may be useful for audit, but they do not help fast operational decisions unless the core bundle is easy to recognise and trust.
Escalate ambiguity before setup becomes sunk cost
If a component is available but its version identity is uncertain, escalation should happen immediately. Once machine time, labour and material are committed, the cost of stopping rises quickly. Fast escalation at the release gate is therefore a cost-control tool as much as a quality-control tool.
Rejected combinations should teach the system something
Every release hold is a signal. If the business repeatedly catches mismatched file and die sets, or outdated substrate allocations, it should review why these near-misses form. The purpose of a release gate is not only to block error but also to show where upstream discipline can improve.
Management checklist
- Confirm the current version identity before action.
- Check which downstream assumptions depended on the previous state.
- Separate obsolete or suspect material physically.
- Assign a clear release or escalation owner.
- Record the impact so the next job benefits from the evidence.
What management should measure
For correct file plate die substrate release, track how often the issue appears, what quantities are placed on hold, the extra setup or proofing time created, and whether the same cause recurs on later jobs. Trend these measures by customer family and process stage so that management can distinguish one-off exceptions from structural weakness. The purpose is not to punish variation; it is to learn where release and version discipline should become stronger.
Frequently asked questions
Is every approved customer change a full restart?
No. The correct response depends on what changed. Some revisions require only a limited revalidation, while others can invalidate tooling, materials or route assumptions and therefore need a much deeper review.
Why are repeat orders still risky?
Because repeat work encourages assumptions. A prior successful run is useful evidence, but it does not prove that the current order still has the same version, material, process and release requirements.
What is the difference between approval and release?
Approval confirms what the customer accepted. Release confirms that the plant has the correct operational combination to execute that accepted version safely and correctly.
Why is shipment proof part of change control?
Because the final question is whether the correct approved version and material actually reached the customer. If that cannot be proven, the change-control chain is incomplete.
Stores and prepress should see the same release status
Many mismatches happen because stores, tooling and prepress each maintain their own local understanding of readiness. A stronger release process lets those functions see one shared status for the job version so that they are not synchronising by phone calls and memory under pressure.
Use setup kits to reduce combination error
Where practical, release the current proof, plate identifiers, die identity and substrate callout as one setup kit or packet. Grouping the combination physically or digitally reduces the chance that operators assemble a run from individually correct but collectively incompatible items.
Re-release rules should be clear after interruption
If the machine stops for a long period, if a shift changes or if suspect output is found, the team should know whether the previous release still stands or whether re-release is required. This protects the plant from assuming that a once-valid setup remains valid after conditions have changed.
Near-miss data should feed standard work
Every time the plant catches a mismatched component before production, it has learned something about where the workflow is vulnerable. Capture that lesson and update the standard release work so that the same vulnerability becomes less likely next time.
Release quality should be visible in startup performance
If the release process is strong, startup should be calmer: fewer surprises, fewer stops for identity questions and fewer emergency calls to prepress or stores. Monitoring startup stability is therefore a practical way to judge whether release discipline is improving.
Shared terminology matters more than many forms
A simple consistent language for versions, release states and setup status can remove a surprising amount of confusion. When every team names the same state differently, even good forms become harder to use under pressure. Shared terminology is a low-cost control with high operational value.
Use one release status across planning, stores and production
A combination is only truly released when the same current status is visible to all functions that supply the setup. If planning sees a new version while stores still issue material against the old packet, the factory remains exposed. A shared release status reduces the need for verbal reconciliation and makes holds easier to enforce. It also gives supervisors a simple rule: if any required component does not point to the same current release, production does not start.
Build a controlled response for last-minute substitutions
Material shortages and tool problems can force substitutions close to startup. The substitution should not bypass the combination check simply because the schedule is urgent. The plant should confirm whether the alternate substrate, tool or route changes colour behaviour, dimensions, finishing compatibility or customer approval requirements. A controlled substitution path allows fast decisions while preserving the logic of the original release gate.
Confirm the released combination again after any setup substitution
During makeready, operators sometimes substitute an available material, alternate die, spare plate or different machine path to recover time. Any substitution should trigger a short compatibility check before production resumes. Confirm that the alternate component still matches the approved version, quality requirement and route assumptions. This prevents a well-intentioned recovery action from quietly creating a new release mismatch.
Make unresolved mismatches visible to planning immediately
If the release gate finds a mismatch that cannot be resolved at once, planning should see the hold immediately rather than discovering it when the machine slot arrives. Early visibility gives the scheduler a chance to move another job, protect capacity and communicate a realistic recovery plan. In this way, strong release control supports schedule reliability as well as quality.