

Two Plants Share a Customer. Which One Owns the Promise?
Multi-plant flexibility can rescue capacity, but only if specifications, revisions, materials, quantities and delivery ownership travel with the job.
The short answer
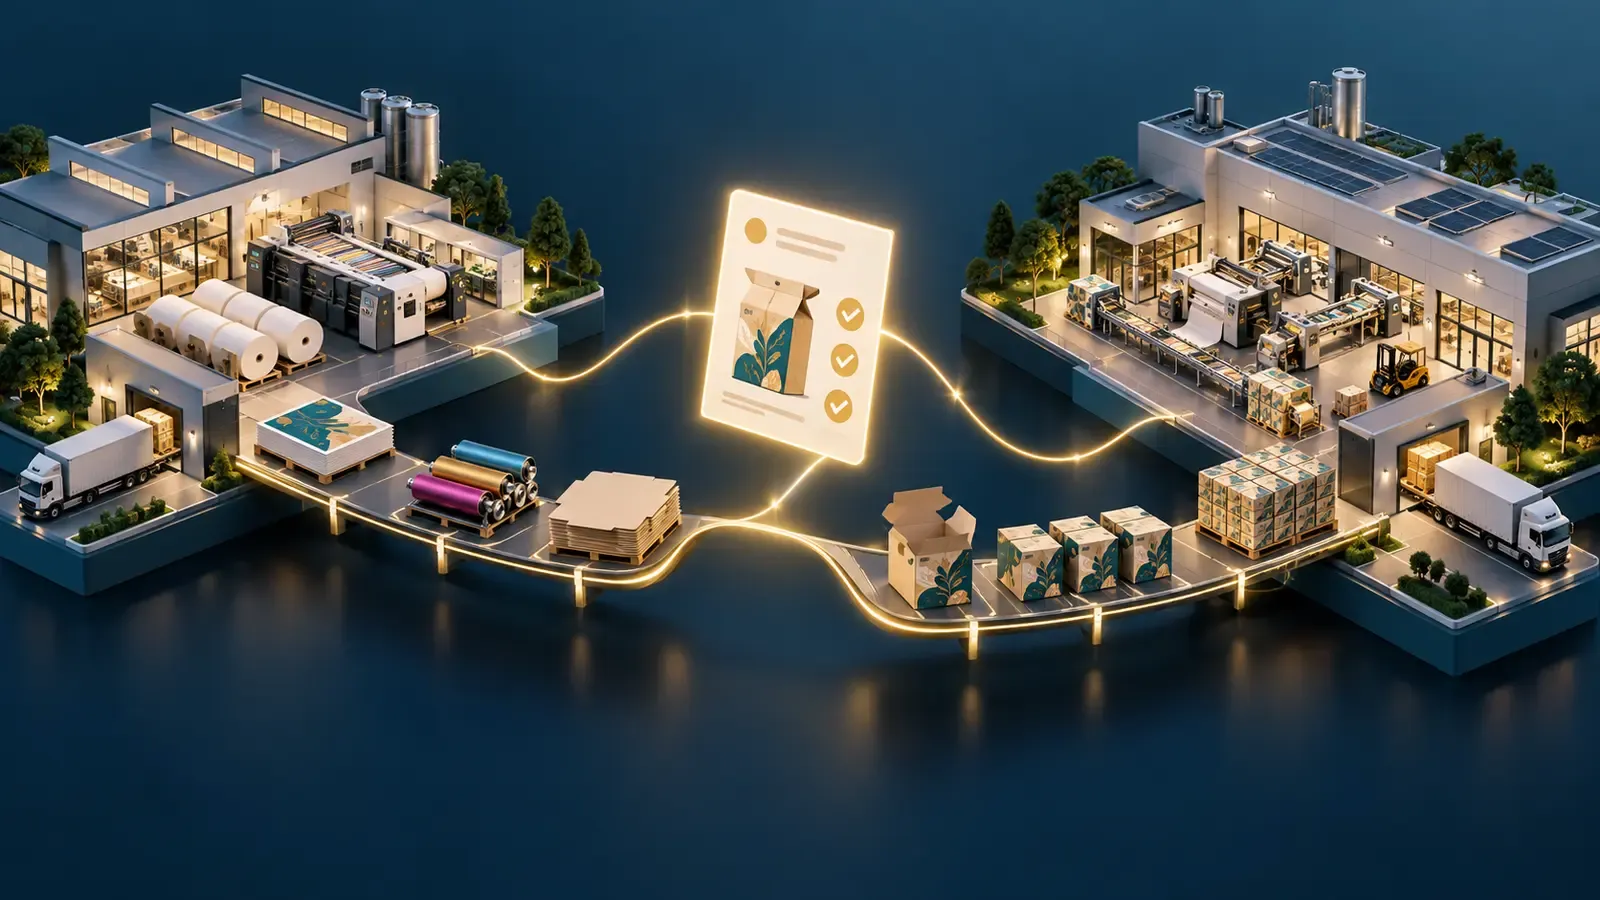
Multi-factory printing works when capacity can move without fragmenting the job. The receiving plant needs the active specification, artwork revision, route, material ownership, quantity state, quality criteria and due milestones. One coordinator must still own the end-to-end customer promise, even when separate plants or legal entities perform the work.
The rescue plan
Plant A loses a critical press for three days. Plant B has compatible equipment and offers to take the urgent jobs. The decision appears obvious.
By the next morning, the transfer list is already uncertain. Plant B uses a different material code for the same board. Its standard spoilage differs. The die has not moved. Customer approval names Plant A. Freight between sites consumes the margin in one short-run job.
Shared capacity created an option, but not yet an executable route.
Transfer capability, not just hours
Two presses with similar descriptions may not be operationally interchangeable. Confirm format, colour configuration, coating, inspection, substrate qualification, tooling, operator skill and customer approval.
Compare the entire remaining route. Moving printing may still leave finishing at the original plant, adding transport and batch-control steps. Moving the whole job may require another supplier, packing method or shipment origin.
The decision should show total lead time, risk and cost—not only the first available press slot.
Create one portable job identity
The job must remain recognisable across sites. Map local item and material codes to one commercial and technical identity. Preserve customer order, active revision, quantity, due date and quality requirements.
Do not solve the transfer by creating an unrelated duplicate order. Duplicates make it easy to lose changes, count output twice or split actual cost.
Where intercompany documents are required, link them to the same controlling job. Local execution can follow each plant’s rules while group management sees one promise.
Move the current truth
The receiving plant needs more than final artwork. Transfer:
- approved file and revision history;
- imposition, plates, dies and tooling status;
- substrate specification, lot constraints and ownership;
- route and operation instructions;
- samples, tolerances and inspection plan;
- quantity already produced, rejected or held;
- packing, labelling and delivery requirements;
- outstanding decisions and named owners.
Confirm receipt and readiness. A file transfer is not an operational handover until the receiver accepts that it can execute.
Decide who owns the promise
Customers should not have to coordinate the group’s factories. Name one order owner responsible for the end-to-end date, specification and communication.
Each plant owns its execution milestones, but the order owner resolves conflicts and presents one answer externally. If the route changes again, that owner makes sure every participant receives the same revision.
This prevents responsibility from falling into the space between sales teams, planners and legal entities.
Plan inter-plant logistics as operations
Material, plates, tools, samples and WIP may travel between sites. Add packing, collection, customs where relevant, receiving and verification to the route.
Identify the last safe departure, not only the expected arrival. Record quantities at dispatch and receipt. Protect sensitive tooling and preserve batch identity.
The capacity planning pillar explains why every dependency must support the delivery promise. A two-hour truck journey can become a lost day when cut-offs and receiving shifts are ignored.
Share capacity with commercial clarity
Intercompany price, material ownership, labour absorption, freight and quality liability affect reported margin. Define them before the emergency becomes an accounting dispute.
The plant that wins utilisation may not be the entity that owns customer revenue. Group profitability matters, but local performance measures should not punish a plant for helping the network.
Preserve actual costs by site and consolidate them to the job. Management can then compare the rescue route with the original plan and learn when multi-plant flexibility creates value.
Standardise selectively
Common product masters, units, reason codes and milestone definitions make transfer easier. Full uniformity is not always necessary.
Standardise the information that must cross the boundary: job identity, revision, quantity states, capability definitions, quality outcome and due evidence. Allow local work instructions where equipment and regulation differ.
This balance avoids two extremes: forcing unlike factories into artificial sameness or accepting data that cannot be compared.
Build a network capacity view
Group planners need qualified capability by plant, not a single number of open hours. Useful attributes include machine format, processes, certified materials, finishing options, tooling location, skills, shifts and transport lead time.
Keep the information current through execution evidence. A theoretical capability unavailable because of maintenance or missing crew should not support a customer promise.
When disruption occurs, planners can screen credible alternatives quickly and then test the complete route.
Review transfer performance
Measure on-time completion, first-pass quality, transfer lead time, quantity variance, extra freight, duplicated setup and total job margin. Also record why the job moved.
Repeated transfers may reveal a structural capacity gap, weak demand allocation or a product family better owned by another plant. Emergency data can improve future network design.
The goal is not to maximise transfers. It is to make the network a dependable option when customer demand and factory reality diverge.
Frequently asked questions
Simulate the transfer before it is needed
Resilience plans often exist only as a list of alternative machines. Test one representative job on paper—or through a controlled production trial. Can both plants interpret the same specification? Are files, samples and tooling available? How will quantities and costs return to the controlling record?
Measure the handoff time, not only the run. The simulation may expose approval clauses, incompatible units, local material codes or transport cut-offs that would remain invisible until a disruption.
Record the verified route and expiry of assumptions. Capability changes when equipment, certification, suppliers or customer requirements change.
Decide what the customer needs to know
Some customers require approval before a manufacturing site changes; others care primarily about specification and delivery. Encode the rule by account and product rather than debating it during each emergency.
Where notification is required, explain how quality, traceability and delivery remain controlled. Preserve the response with the job. The operational team can then execute without uncertainty about commercial authority.
Balance locally, optimise globally
Plant managers naturally protect their own utilisation and targets. Group planning needs a rule for work that creates value across the network but looks inconvenient locally.
Use common definitions for capacity contribution, transfer cost and service result. Credit the receiving plant for genuine support and preserve the full job margin centrally. Transparent rules reduce negotiation when speed matters.
Network flexibility becomes cultural as well as technical: plants share evidence early because they trust how the result will be judged.
Must both plants use identical systems?
No, but shared identifiers and controlled exchanges are essential. Integration must preserve revision, quantity, milestone and cost meaning.
Who approves a plant change?
Authority depends on customer, regulatory and quality requirements. Define when commercial or customer approval is necessary and preserve the decision.
Should material move or be repurchased locally?
Compare availability, qualification, lot requirements, transport, ownership and cost. The fastest physical option is not always the safest specification option.
How should group capacity be measured?
Use qualified capability and realistic route lead time, not the sum of nominal machine hours across sites.
One customer, one answer
Two plants can provide resilience that one plant cannot. The advantage becomes real only when the job crosses the boundary with its identity and evidence intact.
Internally, work may be distributed. Externally, the promise should remain singular: one current specification, one truthful date and one owner who can explain what happens next.
Begin with a capability passport
Create a concise passport for each potential receiving plant: verified processes, formats, materials, certifications, finishing routes, tooling constraints, normal shifts, transport assumptions and local contacts. Date every verification.
Match one representative product family against the passport and identify gaps before an urgent transfer. A missing approved substrate, customer qualification or colour reference may matter more than nominal machine capacity. Close what is practical and record what remains impossible.
During live planning, the passport narrows the search to credible options. The detailed job review still decides whether the transfer works, but teams no longer begin with a phone chain and a list of machine names.
After each transfer, update the passport with actual setup, yield, lead time and handoff lessons. Network knowledge becomes reusable rather than staying with the people who rescued the last order.
That retained knowledge makes the next response faster, safer and easier to cost.