The BOM Changed. The Purchase Order Didn’t.
An engineering revision becomes operational only when every affected demand, purchase, kit, instruction and work order is identified and controlled.
The short answer
An engineering change is controlled only when the factory can identify every affected purchase order, material balance, kit, work order, instruction and finished unit—and then record an authorised decision for each. Updating the BOM master is necessary, but it does not automatically protect transactions already in motion.
Effective engineering change control connects the new product definition to operational exposure before the factory buys, builds or ships the wrong configuration.
The revision was released at 4:17 p.m.
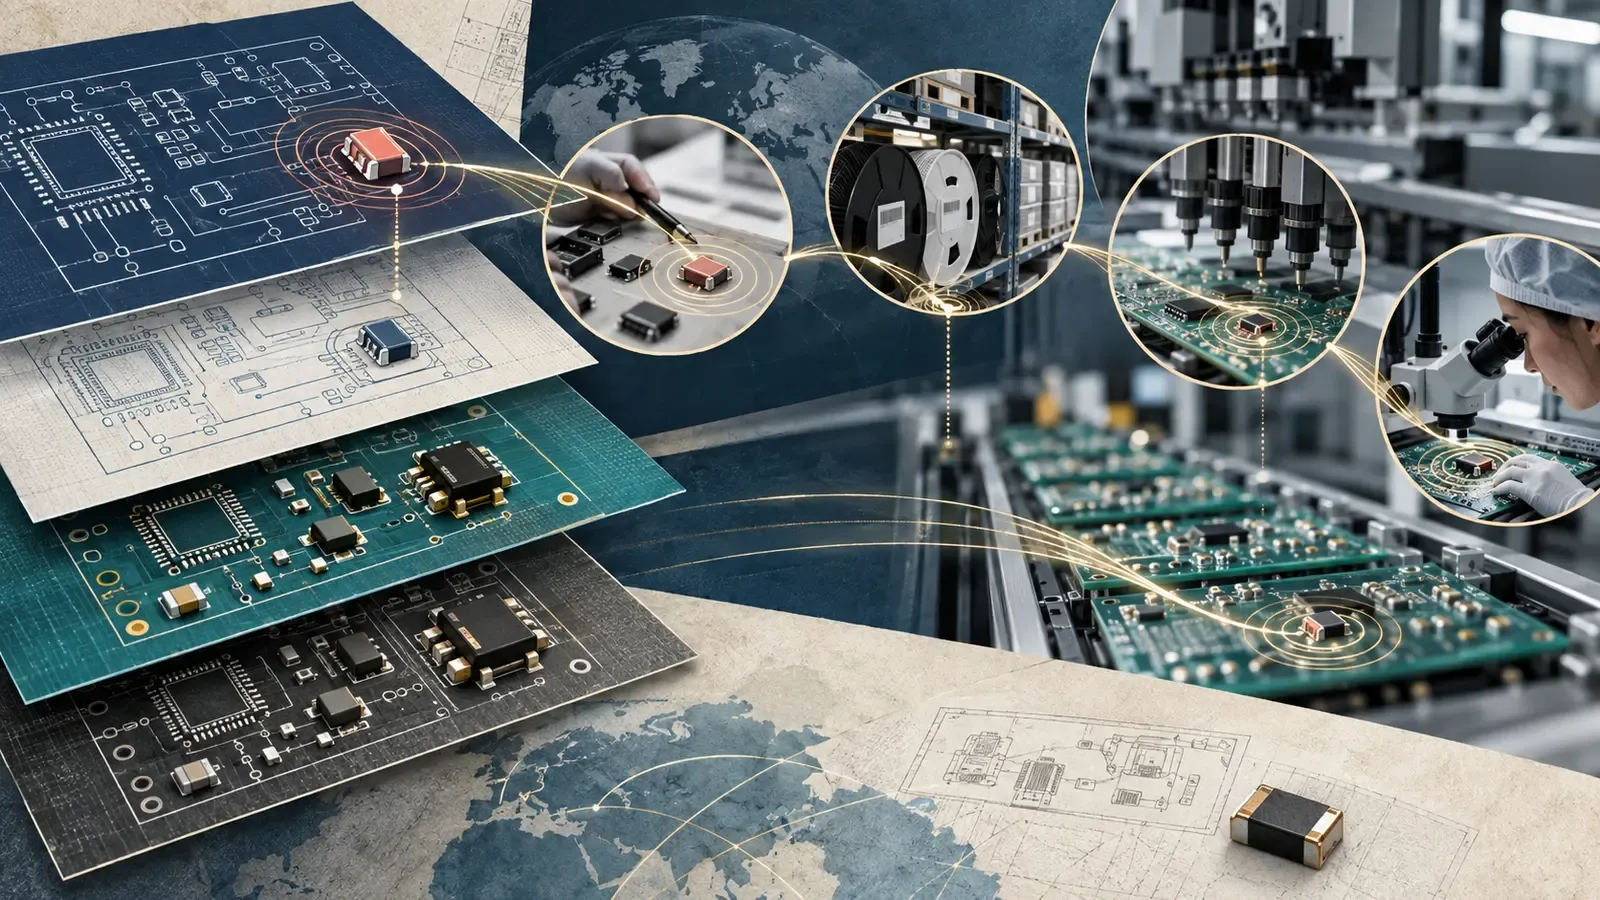
Engineering approves a new capacitor, changes two reference designators and updates the test limit. The revised BOM is correct before the day ends. Purchasing, however, placed orders against the previous requirement last week. Material for three work orders is already allocated. One kit has reached the line. A subcontractor received yesterday’s file.
On the engineering screen, the change is complete. Across the factory, it has only begun.
This gap explains why engineering change control cannot be treated as document administration. A revision changes future truth, while operations contain commitments made under earlier truth. The business must decide exactly where the boundary lies.
Three dates are not one date
Every change needs at least three distinct time concepts.
The release date records when the change became authorised. The effectivity rule defines which demand, date, lot, serial range or work order should use it. The implementation date records when each affected operation actually adopted it.
Confusing these dates creates false confidence. A BOM revised today may apply only to orders built next month. An urgent safety change may apply to all unreleased material immediately. A customer may approve a deviation for one shipment while the permanent revision remains pending.
The system should preserve these differences instead of overwriting history with the newest version.
Start with the reason and risk
Not every change carries the same consequence. A drawing-note correction, alternative packaging label, component substitution and safety-critical circuit change require different scrutiny.
Classify the reason: customer request, lifecycle issue, shortage, cost reduction, quality correction, compliance need or manufacturing improvement. Then identify the risk dimensions: form, fit, function, reliability, regulatory approval, inventory exposure, process instruction and customer notification.
This classification determines the review path. It also helps management see whether frequent changes arise from normal product evolution or weak upstream discipline.
Build an affected-object list
The first operational question is not “Did we update the BOM?” It is “What already depends on the old definition?”
A useful affected-object review includes:
- open quotations and customer orders;
- forecasts and planned demand;
- purchase requisitions and purchase orders;
- supplier acknowledgements and inbound shipments;
- on-hand, quarantined and consigned inventory;
- allocated material and prepared kits;
- released and active work orders;
- subcontract instructions and material;
- finished goods, service stock and units in transit;
- programmes, test limits, drawings and work instructions.
The list should be generated from relationships, not assembled through memory. Each object then receives an action: continue, change, cancel, segregate, inspect, rework, consume under deviation or notify.
The purchase order is part of engineering exposure
Purchasing often sees the internal part number and required date, while engineering sees manufacturer part, revision, approved alternate and effectivity. If those views are not connected, a buyer can satisfy the commercial requirement while violating the technical decision.
When a change affects supply, the buyer needs a clear instruction. Can existing orders continue? Must the supplier change manufacturer or date code? Is old material usable for another product? Will cancellation cost exceed controlled consumption? Does customer approval need to precede commitment?
The change record should capture the decision and link it to the purchase transaction. An email may support negotiation, but it should not be the only evidence explaining why material was accepted or rejected.
Inventory needs disposition, not a red flag
Marking old inventory obsolete does not decide what happens next. Material may be returnable, usable on another revision, acceptable under concession, suitable for service stock or destined for scrap.
Inventory disposition should consider location, ownership, quantity, lot, shelf life, moisture exposure, customer restriction and cost. The same internal part can have different outcomes by lot or site.
Physical control matters. A system hold without clear warehouse identification invites accidental issue. A physical quarantine without an accurate system status leaves planners believing the quantity is available.
Work in progress defines the hard boundary
Changes become most difficult after material has entered production. A panel may be printed but not populated. A board may be assembled but not tested. A unit may be at a subcontractor. The factory needs a process-aware rule for each state.
Ask what can be verified and changed without creating greater risk. Can a component be replaced safely? Does the test programme detect the relevant condition? Must the unit receive a new label or serial relationship? Is a customer concession required?
The answer should attach to the affected work order or serial range. Otherwise, weeks later, the factory knows a change existed but cannot prove which units followed which decision.
Instructions and programmes must change together
A correct BOM does not prevent production from loading an old programme or following a printed instruction left at the station. Product definition includes the complete execution package.
Release controls should align BOM, routing, programme, drawing, tooling data, test limits and operator instruction. Superseded versions should be removed from normal access while remaining available for historical evidence.
At the point of use, the operator should see the valid revision for that work order. The burden should not be on the operator to compare filenames or interpret an email chain.
Use a change board for decisions, not ceremony
A cross-functional review is valuable when it brings together engineering, purchasing, planning, warehouse, production, quality and customer ownership. It becomes wasteful when the meeting only reads a change description.
The board should see exposure by object, quantity, value, location and due date. It should decide effectivity, disposition, verification and communication. Owners and deadlines must be explicit.
Urgent changes need an accelerated path, but not an undocumented path. The higher the urgency, the more important it is to preserve who authorised the temporary rule and when it expires.
Measure implementation closure
Counting released engineering changes says little about operational control. Better measures include time from release to affected-object identification, unresolved exposure by age, quantity built under deviation, obsolete inventory value, repeated emergency changes and discrepancies discovered after release.
Review changes that required expediting, line stoppage, rework or customer explanation. These cases reveal where the decision chain is slow or incomplete.
Closure should mean more than all tasks being ticked. It should mean the factory can explain what changed, why, where the boundary was applied and what happened to every exposed object.
Connect the change to the wider product history
Engineering change is one part of the broader control described in One Product, Hundreds of Decisions. Can Your Factory See Them All?. The revision relationship should continue into material genealogy, production execution, test and shipment.
That connected history allows quality to investigate by actual configuration rather than nominal model. It allows costing to identify obsolete exposure. It allows customer service to explain which shipments contain which revision.
A practical first exercise
Choose one recent change that affected open supply or production. Reconstruct the timeline from request to closure. List every system, spreadsheet, email and physical control used.
Then compare the official effectivity with purchase orders, inventory, kits, work orders and shipped units. Note every point where a person had to infer the correct action. Those inferences are design requirements for the improved workflow.
Do not begin by adding more approval fields. Begin by making affected objects visible and assigning a disposition to each.
Frequently asked questions
Is a new BOM revision enough to control the change?
No. The revision defines the new product, but existing commitments and material require explicit effectivity and disposition. Control includes both future definition and current exposure.
Should every change stop production?
No. The response should reflect risk. Some changes can apply at the next order; others require immediate hold. The decision and its scope must be authorised and recorded.
How should temporary substitutions be handled?
Use a time-, quantity-, lot- or order-bounded deviation linked to approval and affected product. Do not permanently alter the normal BOM to solve a temporary shortage.
Who owns engineering change implementation?
Engineering owns technical definition, but implementation is cross-functional. Purchasing, planning, warehouse, production and quality each own actions on exposed objects.
Can ERP replace engineering judgement?
No. ERP should expose dependencies, enforce effectivity and preserve decisions. Engineers and authorised business owners still determine technical and commercial disposition.
Make the new truth operational
The dangerous change is not the one everyone knows is incomplete. It is the one marked released while old decisions continue invisibly across the factory.
Connect the BOM change to everything that already depends on it. Give each exposure an owner and disposition. Then engineering truth can reach the purchase order, material, work order and shipped product without losing its meaning.