The Components Are in Stock. Why Isn’t the Kit Ready?
Inventory availability is not production readiness when quantities are unallocated, quarantined, on the wrong reel, at another site or missing an approved substitute.
The short answer
Component inventory becomes a production-ready kit only when the required quantity, exact approved identity, quality status, packaging condition, location and timing all match the released work order. “On hand” is an accounting fact. “Ready to issue and consume safely” is an operational fact.
Material kitting control should expose that difference before labour, feeders and line time are committed.
The shortage appears after the kit reaches the line
The planner sees all BOM lines covered. Warehouse prints a pick list. Production reserves a slot. During setup, the team discovers that one reel is at another site, another is under incoming inspection, and a third is approved for a different customer only.
The system did not lie. It answered the wrong question.
Total on-hand quantity cannot describe readiness in electronics manufacturing. Components carry conditions that affect whether they can support this specific order at this specific moment.
Define available, allocatable and ready separately
Available inventory is physically recorded and not fully consumed. Allocatable inventory meets the commercial and technical rules for a demand. Ready inventory can be picked, issued and used within the planned production window.
These states should not be collapsed.
A reel can be available but quarantined. It can be allocatable but located too far away to meet today’s start. It can be ready physically but lack a required certificate. A planned receipt can cover future demand without protecting the immediate kit.
Clear status language prevents teams from arguing over a single number that represents several different realities.
Readiness begins with the released product definition
Kitting against an obsolete BOM creates organised error. Before material is allocated, the work order should identify the valid product revision, approved manufacturer rules, quantity, effectivity and any authorised deviation.
Engineering changes after allocation require an exposure check. Which components remain valid? Which must be removed? Is the replacement in stock? Does the change affect programme, stencil, test or instruction?
The kit should inherit product truth rather than become a frozen snapshot that production must manually reconcile.
Quantity has more than one boundary
The required component quantity includes planned build, panelisation, attrition and any controlled setup allowance. The usable supply side may include full reels, partial reels, floor stock and consigned material.
But gross balance is not enough. Minimum issue quantity, feeder requirements, splice policy, package integrity and remaining count can affect usability. A partial reel with sufficient book quantity may not support the intended uninterrupted run.
Inventory accuracy should therefore be measured at the identity and handling level that production actually needs.
Technical eligibility changes the balance
Approved manufacturer, date code, lot restriction, moisture-sensitivity level, shelf life, bake status, RoHS or other compliance condition can make one balance eligible and another ineligible.
Customer-owned material may not be interchangeable with general stock. A deviation can permit a specific alternate for one order without opening it to all demand. Quality hold should remove stock from the ready quantity even when the material remains physically present.
The kitting view should explain why quantity is excluded. A planner needs an actionable reason, not simply a red shortage line.
Location and time are part of readiness
Material at a remote warehouse may support next week but not a line starting in two hours. Material awaiting an internal transfer is not equivalent to material staged beside production.
Use need-by time at the operation, not only work-order due date. Backward planning can show when each component must be available for kitting, verification and setup.
Transfers should have owner, expected arrival and status. Otherwise planners count the same material as ready while warehouse treats it as future work.
Incoming inspection must be visible to planning
Supplier delivery is not always material availability. Components may require document review, sampling, electrical verification, labelling correction or engineering confirmation.
Planning should see expected release time and risk, while quality sees the production consequence of delay. This connection helps teams prioritise inspection by actual demand rather than receipt sequence alone.
If material is conditionally released, the approval and scope should travel with the lot. Verbal permission should not convert an unresolved condition into unrestricted inventory.
Pick by identity, verify by exception
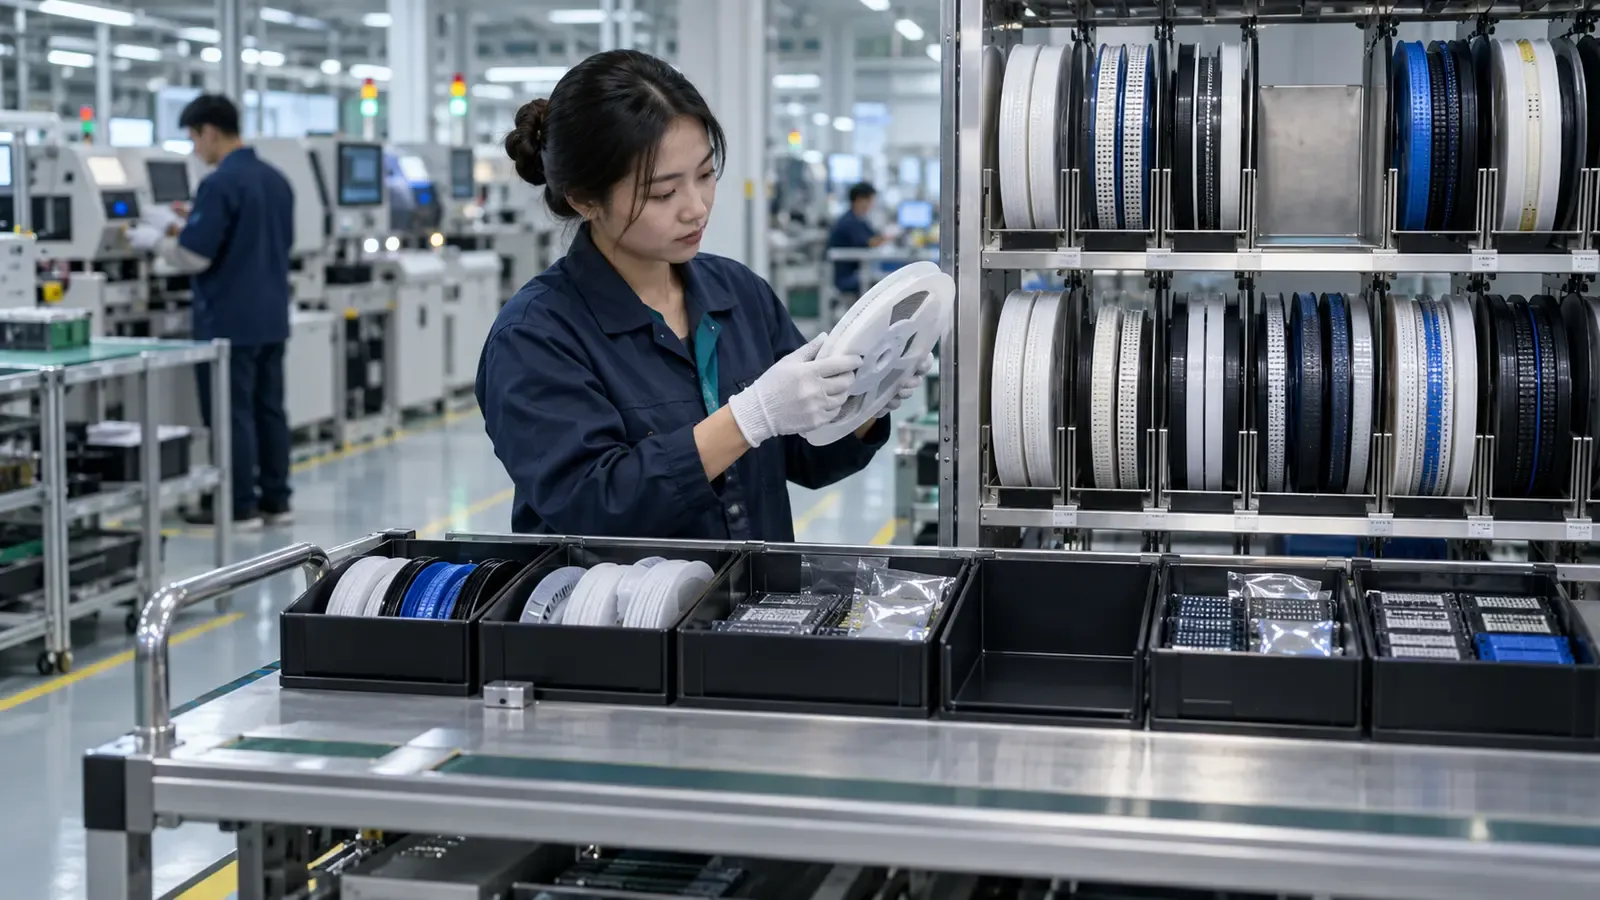
Barcode scanning can confirm item, manufacturer part, lot, location and quantity during pick. The best workflow prevents an ineligible scan and explains the reason immediately.
However, scanning every movement without clear rules creates activity rather than control. Design the process around high-risk mismatches: wrong revision, restricted alternate, expired condition, wrong customer ownership, missing documentation or insufficient remaining quantity.
Operators should not need to memorise approval matrices. The system should translate master-data rules into a simple pick decision.
Preserve partial reels and returns
After production, unused components may return from the line. If lot, manufacturer, remaining quantity or moisture exposure is lost, the returned balance becomes difficult to allocate safely.
Return transactions should preserve identity and condition. Where exposure time matters, record the event needed for the next usability decision. Unknown balance should move to review rather than merge silently with controlled stock.
Cycle counting should include partial reels and common floor-stock practices. Book accuracy that ignores the locations where consumption occurs will not protect kit readiness.
Kit status should be earned
A useful readiness status progresses through defined gates: product released, demand calculated, eligible stock allocated, shortage actions confirmed, material picked, exceptions resolved, kit verified and staged.
Do not allow “complete” because every pick-list line contains a quantity. The status should reflect the technical and physical conditions required to start.
If the kit is partial, show the missing identity, quantity, owner, expected resolution and line consequence. This makes shortage management a controlled queue rather than a daily search exercise.
Connect kitting to the production plan
Kitting and scheduling should share the same readiness evidence. A line slot without a credible kit is not a plan; it is an aspiration.
The related article One Missing Reel Moved the Entire SMT Plan. explains how a single material exception can alter changeovers and downstream capacity. The pillar One Product, Hundreds of Decisions. Can Your Factory See Them All? places material readiness inside the wider product decision chain.
Measure the quality of release
Track kit completion at the planned release time, shortages discovered after staging, substitutions requested under urgency, line stops caused by material and returned quantities with uncertain identity.
Separate supplier shortage from internal readiness failure. Material can be inside the building while the factory still fails to inspect, transfer, allocate or count it in time.
Review recurring shortage reasons by product, component, supplier, location and process owner. The objective is to move discovery earlier.
Run a readiness walk
Select tomorrow’s first work order. Compare the system’s ready quantity with the physical kit and the rules that make each component eligible.
Check revision, manufacturer part, lot, status, location, quantity and packaging condition. Ask what would happen if the order quantity increased, one reel failed inspection or a customer restriction changed.
Every answer that requires a phone call or private spreadsheet points to missing operational context.
Repeat the check after the kit is returned from production. That second view often reveals identity and quantity gaps that the initial pick process cannot show.
Frequently asked questions
Is allocation the same as kitting?
No. Allocation reserves eligible supply against demand. Kitting physically picks, verifies and stages material for execution. Both should use the same product and approval rules.
Should planned purchase receipts count as ready?
They can support future coverage, but they are not physically ready. Show confirmed arrival, inspection and transfer lead time separately from on-hand ready stock.
How should floor stock be handled?
Use a controlled policy based on value, risk and traceability need. The replenishment and consumption method should still support reliable quantity and appropriate genealogy.
Can production start with a partial kit?
Sometimes, under an authorised decision that considers sequence, interruption risk and downstream impact. The exception should be visible and owned.
Who owns kit readiness?
Planning coordinates the requirement, while engineering, purchasing, quality and warehouse own conditions that affect eligibility. Production confirms the kit can execute the planned operation.
Make “ready” mean ready
A factory does not benefit from optimistic inventory if the line cannot safely consume it. Connect quantity to revision, approval, condition, location and time.
When kit status is earned through those conditions, planners can commit capacity with confidence and warehouse teams can focus on real exceptions before they become line stoppages.