

The Parts Are in Stock. Why Is the Work Order Still Not Ready to Build?
Inventory on hand does not guarantee an EMS work order is build-ready. Correct revision, approved source, lot status, quality release, allocation, quantity and location all matter before material can support production.
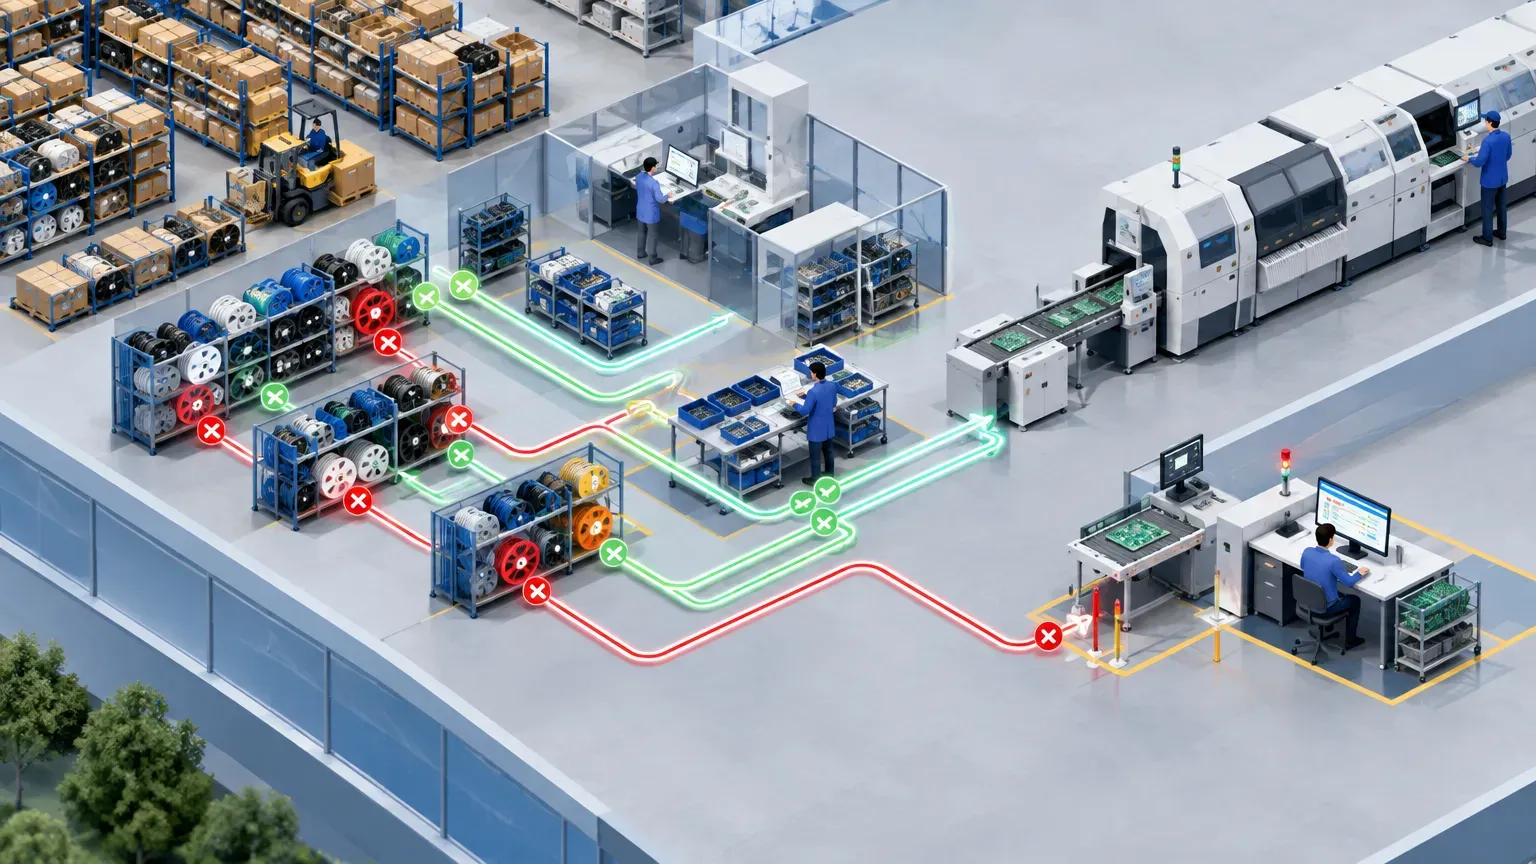
The short answer
An EMS work order is material-ready only when the required components are not just present in inventory but usable for that exact build. Correct BOM revision, approved manufacturer, quantity, allocation, location, quality status and traceability condition all matter. A warehouse balance can therefore look healthy while production still cannot start.
The same question belongs to the wider From RFQ to Production Ready: What Does an EMS Manufacturer Need to Control? operating picture: material readiness has to remain connected to the decisions made before and after it, rather than becoming a separate local control.
Quantity on hand is only the first test
ERP can show that the item quantity exists.
The next questions are:
- Is it allocated?
- Is it at the right site?
- Is the lot released?
- Is the manufacturer approved?
- Is the part valid for this BOM revision?
- Is enough quantity available for expected attrition?
Only then does inventory become production-ready supply. Use the current BOM revision. A kit prepared for revision A may be wrong after revision B is approved.
Material readiness should be calculated against the current effectivity.
If an ECN replaces a component, the old part may remain physically available but no longer be valid for new production.
This is why engineering and material status cannot operate independently.
Account for approved alternates. Material readiness can improve when an approved alternate is available.
The planning model should know whether the alternate can satisfy demand.
But it should not assume every generic equivalent is usable.
Approved-source logic should feed readiness. Include quality status. Received material may be in inspection or quarantine.
Treating that stock as fully available can create false readiness.
Planning should distinguish unrestricted, inspection, hold and rejected status as appropriate.
This avoids releasing work that depends on material quality has not yet released. Check lot or date-code requirements. Some electronics customers impose date-code, shelf-life or lot restrictions.
Material can be on hand but unsuitable for the specific job.
Where these rules apply, readiness should reflect them.
The system should support the required control without adding restrictions where they are not needed.
Consider moisture-sensitive and handling state
Some components require controlled storage and floor-life handling.
The relevant operational state may affect whether material can be issued or needs preparation.
This is a good example of industry execution detail that sits beyond a simple inventory balance. Protect customer-owned inventory. Consigned material may belong to a specific customer or program.
Do not treat it as general supply simply because the internal item number matches.
Ownership and allocation need to remain visible.
This is especially important in EMS environments serving multiple customers with similar components. Use kit shortage by criticality. A work order can have 99% of lines available and still be impossible to start.
Count of shortage lines is less useful than identifying the component that blocks the first executable operation.
Classify critical shortages by impact.
This focuses procurement and planning attention on what actually stops production.
Separate full-kit and staged-kit models. Some factories require complete kits before release.
Others allow production to begin when early operations are covered and later material will arrive in time.
Both can work.
The important requirement is an explicit readiness rule.
Otherwise different planners release work according to personal judgment.
Connect readiness to schedule
A schedule filled with non-ready jobs becomes unstable.
Before constrained SMT or assembly capacity is committed, confirm the relevant material rule.
This protects machine time from jobs that cannot execute.
It also improves customer promise reliability. Make shortage ownership visible. Each critical shortage should have:
- responsible buyer/planner;
- expected recovery;
- approved alternate status;
- customer decision if required;
- affected work order.
This converts a shortage list into a recovery process. Consider attrition and feeder/setup quantity. SMT and electronics assembly can require component quantity beyond theoretical BOM demand.
Setup, feeder loading, machine handling and normal process attrition can influence the required quantity.
Material readiness should use the factory's realistic requirement rather than exact BOM multiplication where additional quantity is operationally necessary.
Review shared components across customers. A common component may serve several programs.
During shortage, allocation becomes a management decision.
The system should show competing demand and customer restrictions clearly enough that planners do not unintentionally consume stock reserved for a higher-priority or restricted order.
Distinguish shortage from information gap
Sometimes material exists but the system cannot prove whether it is approved, inspected or allocated correctly.
That is not a physical shortage.
Classify these cases separately.
Reducing information gaps can improve production readiness without buying one additional component. Include feeder and packaging form. The right electronic component in the wrong packaging form can still create production difficulty.
Reel, tray, tube and other forms may affect line setup or equipment compatibility.
Where the manufacturing process requires a specific form, material readiness should include that requirement.
This is another reason internal part quantity alone can be misleading. Confirm programming and firmware dependencies. Some components or assemblies require programming before or during production.
A work order may have all physical parts but still not be executable if firmware, program files or programming equipment are not ready.
Include these dependencies in production-readiness rules for relevant products.
Measure shortage recovery quality. A shortage can be recovered through expedited supply, alternate approval, allocation change or schedule movement.
Track the recovery method.
If the same part repeatedly requires expediting, the issue may be planning or sourcing strategy rather than random shortage.
If deviation approval is repeatedly required, engineering may need a permanent alternate.
Make material readiness visible before the shift starts
A readiness review is most valuable before operators and machines are waiting.
For near-term work, show critical shortages, held lots, missing approvals and incomplete kits early enough for purchasing, quality or planning to recover.
This reduces the common pattern where the ERP schedule looks executable until the first component scan fails at the line. Use readiness history to improve planning parameters. If the same components repeatedly arrive too late, the issue may be lead time, safety stock, MOQ strategy or supplier reliability.
If jobs repeatedly wait for inspection, quality capacity may be the constraint.
Material-readiness data should therefore feed planning improvement rather than remain only a daily shortage report.
Distinguish customer-priority allocation from automatic allocation. During shortage, management may choose to reserve limited components for a strategic or time-critical order.
That is a business decision.
The system should preserve the resulting allocation so another planner or warehouse user does not unknowingly consume the stock elsewhere. Use readiness categories that operators understand. A simple status such as Ready, At Risk or Blocked can be more useful than a long shortage report if the reason is visible underneath.
For blocked work, show whether the constraint is material quantity, source approval, quality, revision or another dependency.
Clear categories help supervisors sequence executable work without interpreting raw inventory data.
It also gives management a cleaner measure of why planned work fails to become executable on time.
What management should measure
Useful indicators include:
- released jobs with critical shortages;
- material on hand but unusable;
- shortages caused by quality hold;
- shortages caused by wrong revision;
- shortages caused by source restriction;
- consigned material conflicts;
- days between material readiness and planned start;
- schedule changes caused by material.
These measures show whether production delay comes from supply quantity or control state.
A practical review
Pick five work orders that were delayed despite apparently sufficient inventory.
Trace the first blocking component.
Classify whether the cause was quantity, revision, source approval, quality, allocation, location or traceability status.
The pattern will show which readiness rule needs improvement.
Where Epicor Mars fits in material readiness
For material readiness, the key system-design question is how to keep enterprise control and electronics-specific execution on the same operating thread. Epicor provides the enterprise-grade ERP foundation for customer orders, purchasing, inventory, planning, costing, finance, approvals and governance. Epicor Mars extends that foundation with the EMS industry context needed at the point of work, including material identity and readiness.
That connection is directly relevant to The Parts Are in Stock. Why Is the Work Order Still Not Ready to Build?. Inventory on hand does not guarantee an EMS work order is build-ready. Correct revision, approved source, lot status, quality release, allocation, quantity and location all matter before material can support production. When the Epicor Mars execution record stays tied to the Epicor work order, material and customer context, management can compare the business commitment with what the factory actually executed without maintaining a second source of truth.
For material readiness, that complementary positioning is the point: Epicor remains the enterprise-grade foundation, while Epicor Mars adds the EMS workflows needed to make this particular control operational on the factory floor. Explore Epicor Mars for electronics manufacturing.
Frequently asked questions
Does material readiness require 100% kit completion?
Not always. It depends on the production model and routing. The rule should be explicit.
Can quality-inspection stock count as available?
Only according to the company's controlled planning policy. It should not silently appear equivalent to released stock.
Should approved alternates automatically satisfy shortages?
Only where the alternate is valid for that customer/product/revision and the required approval is complete.
Why can inventory be high while production is short?
Because ownership, allocation, revision, source and quality can make physical stock unavailable to the specific work order.