

A Defect Reached the Customer. Can Your EMS Operation Contain It Fast Enough?
Customer escapes in electronics manufacturing are managed well only when quality, genealogy, material identity, WIP, supplier history, rework and shipment records can be connected quickly enough to define the real affected population and corrective action.
The short answer
An EMS quality escape is contained effectively when the business can identify what failed, which exact product and revision were affected, what material and process history sits behind the failure, which other units may share the same risk, and what immediate action prevents further shipment. The speed of that response depends less on having more quality forms and more on having one connected manufacturing record.
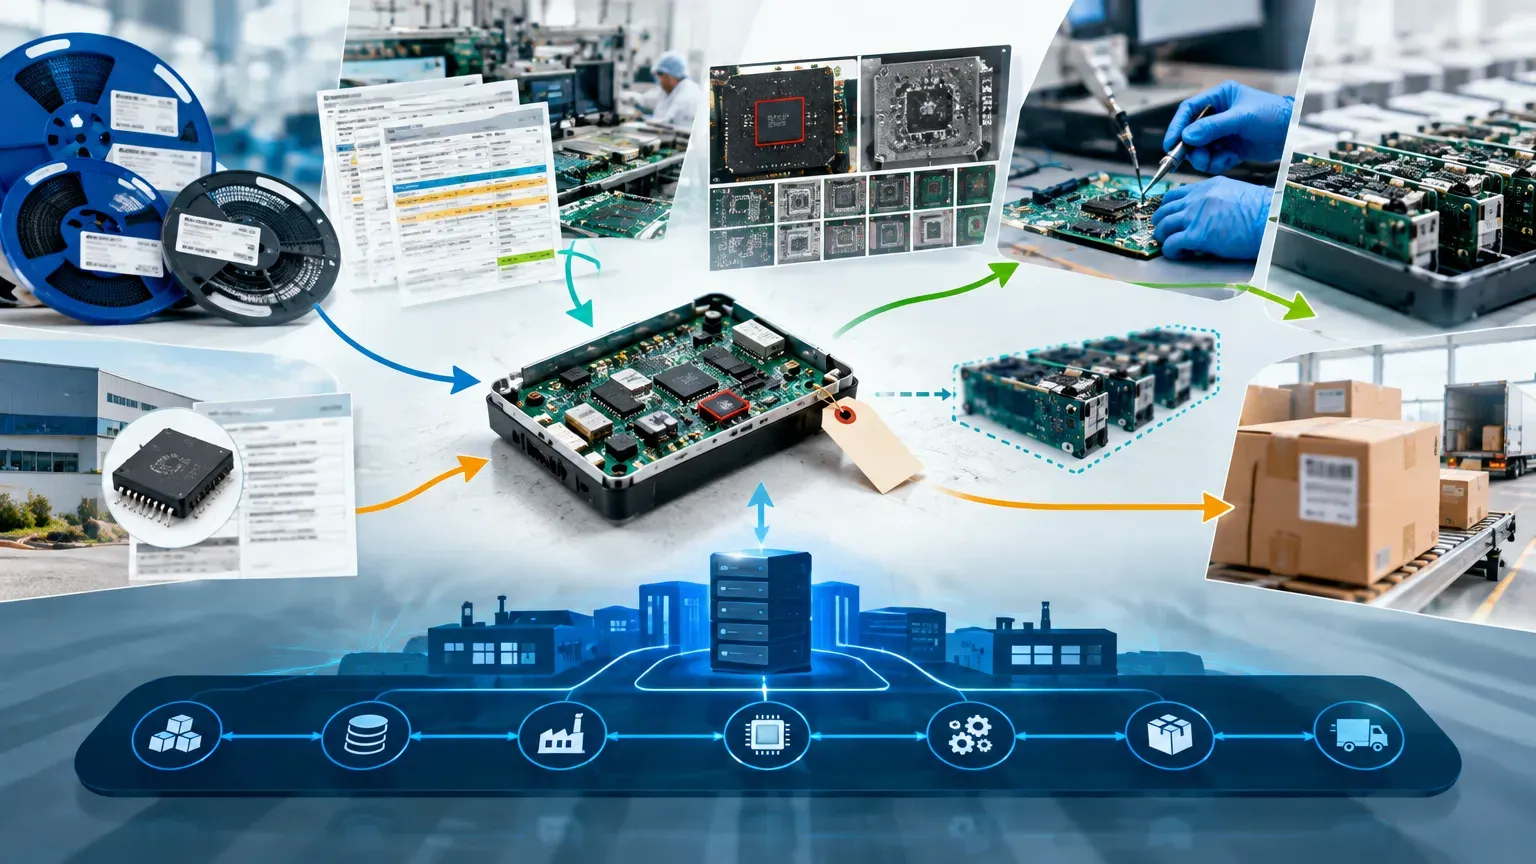
For electronics and EMS operations, that record can span supplier source, component lot, incoming inspection, work order, operation, machine or station, AOI/test result, rework, finished serial, packing and shipment.
This is where the ACC architecture matters. Epicor provides the enterprise-grade ERP foundation for purchasing, inventory, orders, planning, costing, finance and governance. Epicor Mars adds the electronics/EMS industry execution layer around material identity, barcode-driven transactions, shop-floor status, quality and genealogy. When those layers remain connected, quality containment becomes an operational process rather than an investigation built from spreadsheets and email.
Customer escape is a population problem
When one customer reports a failed unit, the first instinct is often to focus on that unit.
Management also needs to ask a wider question:
How many other units could share the same cause?
The answer may depend on:
- the same component lot;
- the same approved manufacturer;
- the same supplier shipment;
- the same production line;
- the same program or test revision;
- the same work order;
- the same rework method;
- the same shift or process window;
- the same shipment.
Containment is the discipline of finding the smallest defensible affected population quickly enough to act.
If traceability is weak, the organization may be forced to hold far more product than necessary.
Start with the returned or failed unit. The investigation needs one controlled anchor.
That may be:
- finished serial;
- work order;
- production lot;
- RMA number;
- shipment reference.
From that point, the team should be able to reconstruct the relevant manufacturing history.
This is why genealogy captured during normal execution matters.
A quality team cannot create reliable genealogy after the fact if material identity was lost on the shop floor. Supplier quality begins before inspection. Incoming inspection is useful, but it is only one control.
A component can pass sampling and still contain latent or intermittent defects.
A supplier can be technically approved while one lot performs poorly.
A manufacturer part can be valid while the source used for a particular shipment creates risk.
A Component Passed Receiving. Why Did Supplier Quality Still Reach Production? examines how approved-source control, lot identity, inspection evidence and forward trace need to work together.
Nonconformance needs an immediate disposition path. When a defect is found on the line, production needs to know what to do with the affected unit, material and potentially related WIP.
The options can include:
- stop;
- quarantine;
- inspect;
- rework;
- use under deviation;
- scrap;
- return to supplier;
- continue unaffected quantity.
A Defect Was Found on the Line. Should Production Stop, Rework or Continue? looks at the MRB and containment decisions that keep abnormal work from becoming uncontrolled work.
Detection point is not root cause
AOI may detect a solder defect.
Functional test may detect an electrical failure.
Final inspection may detect the wrong label.
These detection points tell the business where the problem became visible, not necessarily where it was created.
AOI Found the Defect. Where Was the Defect Actually Created? explains why useful quality analysis connects the detection event back to the creating process, material, program or handling condition. Corrective action needs recurrence evidence. A supplier can submit a corrective-action report that looks complete.
The more important question is whether later lots behave differently.
A strong closure process asks:
- Was containment effective?
- Was the true cause addressed?
- Was the process change implemented?
- Did later receipts improve?
- Did the same defect recur?
Supplier Corrective Action Closed. How Do You Know the Problem Will Not Return? focuses on closing the loop with evidence rather than paperwork alone.
RMA needs both backward and forward trace. Customer return analysis usually starts backward:
What components, lots, process and test history belong to this serial?
Once a suspect cause is found, the investigation moves forward:
Which other units used the same lot, process or condition?
The Customer Returned One Unit. How Many More Could Be Affected? covers that two-way trace. Quality has an economic footprint. A defect can create more than scrap.
It can also create:
- rework;
- retest;
- additional inspection;
- premium freight;
- customer return handling;
- supplier recovery work;
- engineering time;
- production disruption;
- line downtime;
- delayed shipment.
Quality Cost Is Rising. Which Failures Are Actually Driving It? explains how these effects can be connected to the originating defects and jobs.
Build a containment sequence
When a material quality event appears, a practical sequence is:
1. identify the observed failure;
2. define the suspected common factor;
3. stop or hold the exposed population;
4. identify where affected material/WIP is located;
5. prevent further consumption or shipment;
6. inspect or test where evidence justifies it;
7. release unaffected product deliberately;
8. start root-cause analysis.
The containment action should be proportionate.
Over-containment wastes working capital and capacity.
Under-containment risks another escape. Use genealogy to narrow the scope. Suppose a returned unit contains a suspect IC.
Good genealogy may show:
- manufacturer;
- supplier;
- lot/date code;
- receipt;
- inspection status;
- work order;
- material issue;
- finished serials.
The business can then identify exactly which production used the same lot.
Without that history, the team may need to hold every unit of the same product or time period.
The value of genealogy is therefore not just compliance.
It is decision precision.
Preserve as-built history after rework. A repaired unit may no longer contain its original component.
If genealogy is not updated, the investigation can point to the wrong material.
Epicor Mars-style execution should preserve the actual as-built state where traceability requirements justify it.
This includes replacement component, repair event and retest result.
The quality record must describe the delivered product, not only the first build attempt. Keep quality status connected to inventory. Suspect material should not remain indistinguishable from unrestricted inventory.
The enterprise record needs clear status for:
- inspection;
- hold;
- rejected;
- approved deviation;
- released.
Epicor can provide the enterprise inventory and purchasing control while Epicor Mars carries electronics-specific material identity and execution context.
This connection prevents production from consuming stock that quality has already restricted.
Separate immediate containment from root cause
Containment stops the problem from spreading.
Root cause explains why it happened.
Corrective action changes the system so recurrence becomes less likely.
These are different steps.
A 100% inspection can be excellent containment and still be a poor permanent solution.
Management should know which stage an issue is in. Use defect families that support action. Defect codes should help improvement.
A list containing only “fail” and “pass” is too weak.
A list with hundreds of rarely used codes can be equally unusable.
Useful defect families can include:
- component;
- solder;
- placement;
- polarity/orientation;
- programming;
- test;
- mechanical;
- labeling;
- cosmetic;
- handling.
The exact taxonomy should match the manufacturing process.
Connect defects to process evidence. When a defect recurs, look for common evidence:
- line;
- operation;
- machine;
- program revision;
- material lot;
- operator/shift where relevant;
- fixture;
- rework method.
The objective is not to blame the closest person to the defect.
It is to identify the control that should change. Use MRB decisions as learning data. Material Review Board or equivalent disposition decisions can reveal recurring weakness.
If the same component is repeatedly accepted under deviation, perhaps the specification, supplier or approval model needs review.
If the same solder defect repeatedly goes to rework, perhaps the process needs engineering action.
MRB should not become a permanent bypass route around root-cause work.
Include supplier corrective action in the same evidence chain
Supplier quality should not live in a disconnected database if the manufacturing record contains the evidence.
A supplier corrective action can link:
- supplier;
- manufacturer;
- part;
- lots;
- receiving defects;
- production defects;
- customer complaints;
- containment quantity.
This gives sourcing and quality a much stronger basis for supplier review. Use customer return evidence to improve production. RMA findings should flow back to:
- engineering;
- supplier quality;
- production;
- test;
- repair;
- work instructions;
- inspection.
If the returned unit reveals a process weakness, update the operating baseline.
A customer complaint should not end with replacement shipment alone. Measure containment speed. Useful time measures include:
- time from complaint to affected-unit identification;
- time to first hold;
- time to complete forward trace;
- time to supplier containment;
- time to disposition affected WIP;
- time to customer response.
Fast response depends on data availability and decision ownership.
It should not depend on heroic manual searching.
Measure recurrence, not only closure. A quality issue can be marked closed and still recur.
Track defect family after corrective action.
If the same failure returns, review whether:
- the cause was wrong;
- the action was incomplete;
- implementation was weak;
- another cause exists.
This is more useful than counting closed CAPAs alone.
Keep enterprise financial impact visible
Quality action has business consequences.
Scrap affects inventory and cost.
Rework consumes labor.
Supplier recovery may create debit or credit.
Customer returns affect service and logistics.
Epicor provides the enterprise-grade financial and transaction context needed to see these effects.
Epicor Mars provides the manufacturing detail that explains the cause.
Together they connect quality improvement with business performance. Containment should include physical, digital and commercial boundaries. A quality escape can spread through more than physical inventory. The organization may also have released a production program, test limit, approved alternate or work instruction that carries the same risk into future work. During containment, review not only stock and WIP but also the digital and process conditions that could recreate the defect. Commercial boundaries matter too. If the same product is built for several customers under different approval rules, the affected population may not be identical across accounts. Containment is strongest when the team defines the physical units, process conditions, data revisions and customer commitments that must be frozen or reviewed.
Use containment ownership by location. Suspect material may exist in receiving, warehouse, line-side storage, WIP, rework, finished goods, subcontractor stock and customer shipments at the same time. Assign an owner to each location class. This avoids the common problem where everyone assumes another department has contained the material. The quality leader may coordinate the event, but warehouse, production, subcontract management and customer service each need a clear action. A simple location-by-location containment checklist makes the status visible and helps management know when the business has truly stopped additional exposure.
Build trace tests into normal operations. The first time a company tests genealogy should not be during a major customer complaint. Run periodic mock trace exercises. Pick one finished serial and trace backward to selected critical lots. Then select one lot and trace forward to every WIP, finished unit and shipment that used it. Time the exercise and note every manual lookup. The purpose is not to prove perfection. It is to find where barcode identity, transaction timing, rework history or shipment linkage still breaks. Those gaps can then be improved before a real containment event puts the organization under time pressure.
What management should measure
Useful indicators include:
- customer escapes;
- incoming supplier defects;
- production nonconformances;
- containment response time;
- forward-trace completion time;
- WIP on quality hold;
- rework rate;
- repeat defect rate;
- supplier corrective-action recurrence;
- RMA by defect family;
- cost of poor quality;
- units released under deviation;
- traceability gaps discovered during investigation.
The point is not to create a larger quality dashboard.
The measures should help management decide where risk and economic loss are recurring.
A practical customer-escape review
For one recent customer escape, ask:
1. Which exact unit or lot failed?
2. What product and revision was it?
3. What suspect material/process factor was identified?
4. Which other WIP or shipped units shared that factor?
5. How quickly were they located?
6. What was contained?
7. What was released?
8. What was the root cause?
9. What corrective action changed?
10. Has recurrence been checked on later production?
If any answer required reconstructing the story from email or spreadsheets, the quality system has an integration gap.
Where Epicor Mars fits in quality containment and closed-loop control
For quality containment and closed-loop control, the key system-design question is how to keep enterprise control and electronics-specific execution on the same operating thread. Epicor provides the enterprise-grade ERP foundation for customer orders, purchasing, inventory, planning, costing, finance, approvals and governance. Epicor Mars extends that foundation with the EMS industry context needed at the point of work, including material identity and readiness.
That connection is directly relevant to A Defect Reached the Customer. Can Your EMS Operation Contain It Fast Enough?. Customer escapes in electronics manufacturing are managed well only when quality, genealogy, material identity, WIP, supplier history, rework and shipment records can be connected quickly enough to define the real affected population and corrective action. When the Epicor Mars execution record stays tied to the Epicor work order, material and customer context, management can compare the business commitment with what the factory actually executed without maintaining a second source of truth.
For quality containment and closed-loop control, that complementary positioning is the point: Epicor remains the enterprise-grade foundation, while Epicor Mars adds the EMS workflows needed to make this particular control operational on the factory floor. Explore Epicor Mars for electronics manufacturing.
Frequently asked questions
Does better traceability prevent defects?
Not by itself. It improves containment and investigation. Prevention still requires process, supplier and engineering improvement.
Should every customer return trigger a full CAPA?
Not necessarily. Use risk, recurrence and customer requirements to decide the level of corrective action.
Is incoming inspection enough for supplier quality?
No. Inspection is one control; approved source, supplier performance, lot trace and corrective action are also important.
Why connect quality to Epicor?
Because inventory, purchasing, orders, costing and financial exposure are enterprise transactions. Epicor Mars adds the EMS-specific manufacturing evidence behind them.
What is the first thing to improve?
Run one mock trace from a finished serial backward to critical component lots and then forward from one suspect lot to all affected units. The manual gaps will be obvious.