One Missing Reel Moved the Entire SMT Plan.
A schedule is only executable when materials, programmes, tooling, feeders, people and downstream capacity agree at the same moment.
The short answer
An SMT schedule is credible only when the planned sequence is executable with the actual reels, feeders, programmes, stencils, tooling, people, machine state and downstream capacity available at the required time. One missing component can change more than one job because resequencing creates new changeovers and shifts constraints through the factory.
Good scheduling connects finite capacity with live readiness and records why the plan changed.
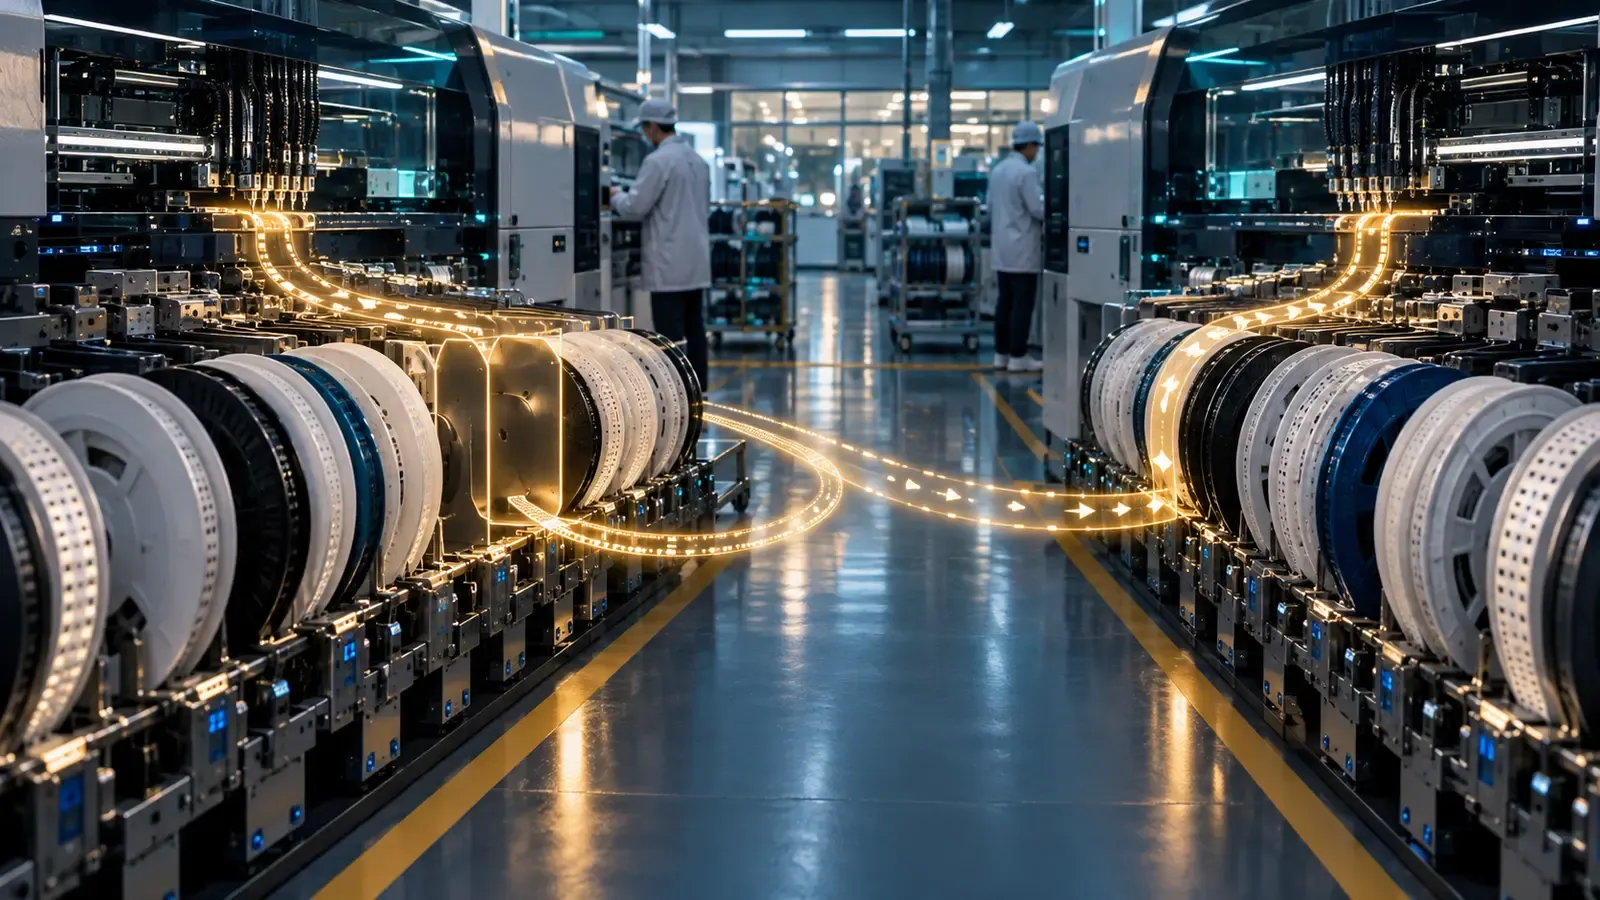
The line was ready except for one reel
Operators complete the changeover. The programme is loaded, stencil verified and feeders prepared. One component reel cannot be found in the staged kit. The next job has material, so supervision moves it forward.
The decision protects immediate utilisation, but its consequences travel. The replacement job needs a different setup. Inspection receives an unexpected mix. A downstream manual process becomes overloaded. The delayed customer order loses another day because its recovered slot is no longer simple.
The missing reel did not merely delay one operation. It changed the network of commitments around the line.
Capacity is conditional
A line may have eight hours open on the calendar, but not every product can use those hours. Machine capability, component package, board dimensions, feeder capacity, programme status, tooling, operator skill and maintenance condition affect eligibility.
Finite scheduling should model the constraints that materially change execution. It does not need to represent every physical detail, but it must distinguish a theoretically open line from a line that can run this job.
The more frequently supervisors override the plan for the same reason, the stronger the case for making that constraint visible upstream.
Material readiness belongs inside scheduling
Traditional planning can create work orders from demand and calculate shortages separately. SMT execution needs the two views to converge.
A scheduled job should show whether every critical component is allocated, picked, verified and expected at the line before setup. Planned receipts need realistic receiving, inspection and transfer time. Approved alternates should reflect the specific product and customer.
The article The Components Are in Stock. Why Isn’t the Kit Ready? explains why on-hand quantity cannot represent executable supply.
Sequence has a setup cost
Two jobs with identical run time can impose very different changeover burdens. Product family, board type, stencil, feeder arrangement, component commonality, programme and inspection setup influence transition time.
Grouping compatible jobs can increase productive capacity, but excessive grouping may delay urgent orders or build inventory early. The schedule must balance setup efficiency with customer priority, material risk and downstream flow.
Record actual changeover duration and reason. Without that evidence, planners use standard assumptions while the factory repeatedly pays for unmodelled complexity.
The bottleneck can move during the day
SMT placement may appear to be the centre of the schedule, yet inspection, test, coating, manual assembly or rework can constrain the order. Running the placement line faster can simply create a larger queue.
Look at the complete routing and current work in progress. A job should not move forward solely because SMT capacity is available if its downstream step cannot absorb the output within the required window.
This is especially important for mixed-volume EMS environments, where product routes and test requirements vary widely.
Freeze windows need a controlled release valve
A short-term freeze window protects execution from continuous replanning. Inside that window, changes should require an explicit operational reason: material failure, machine breakdown, urgent customer priority, quality hold or constraint recovery.
The freeze should not prevent necessary action. It should make the consequence visible and ensure an authorised person accepts it.
Outside the window, planning can optimise sequence more freely. Clear boundaries reduce the cycle in which every department believes a different version of the schedule.
Use readiness gates before setup
Before a job enters the frozen execution sequence, verify product revision, programme, stencil, feeder plan, tooling, kit, quality documents, people and downstream capacity.
Readiness can be represented as a small set of gates with owners and due times. A red gate should explain the issue and recovery plan. A green gate should mean the condition has been verified, not merely assumed.
This makes the pre-production meeting shorter and more decisive. Teams discuss unresolved exceptions instead of reading every order aloud.
Respond to breakdown with scenario choices
When a machine stops, the schedule needs more than a new finish time. Which jobs can move to another line? What qualification or programme verification is required? Which setup is already prepared? What downstream promise changes?
Scenario planning can compare options by lateness, changeover, material movement and constraint impact. Even a simple structured comparison is better than moving the loudest customer first.
Record the selected reason. Historical schedule changes reveal whether instability comes from maintenance, material, engineering, quality, customer priority or planning assumptions.
Connect actual execution to the next plan
MES evidence should update start, stop, quantity, scrap, downtime and completion. The scheduling view then works with current reality rather than yesterday’s report.
Avoid false precision. If operators report completion late or machine signals are unreliable, the plan will appear accurate while decisions remain stale. Data timeliness is part of schedule quality.
Use a clear fallback when automatic capture fails, and review gaps instead of silently filling them with assumed times.
Measure adherence by reason
One percentage for schedule adherence cannot explain improvement. Separate variance caused by missing material, engineering release, programme or tooling, machine downtime, staffing, quality hold, downstream congestion and customer reprioritisation.
Measure when the issue became knowable. A component shortage identified three days before start is different from one discovered after changeover. Both affect adherence, but only the second indicates a readiness failure at release.
Review repeated causes with the team that owns the upstream decision.
Protect customer promise from local optimisation
High machine utilisation can be achieved by running whatever is ready, even if the sequence weakens priority and creates excess work in progress. The factory can look busy while late orders become later.
Schedule objectives should reflect customer promise, flow, setup, constraint use and risk. No single measure should dominate every situation.
The broader pillar One Product, Hundreds of Decisions. Can Your Factory See Them All? explains why planning needs shared product, material and execution identities.
Run a one-day schedule autopsy
Take yesterday’s frozen plan and compare it with actual sequence. For every change, capture when the problem was first visible, who decided, why the job moved and what downstream effects followed.
Then identify the three most frequent avoidable changes. Improve their readiness rule, data source or ownership. Do not begin by buying a more sophisticated optimiser if the inputs remain unreliable.
Repeat weekly until schedule change becomes an explainable exception rather than the normal operating method.
Make planning assumptions visible
Every schedule relies on assumptions about run rate, setup, yield, staffing, material arrival and downstream availability. Store the important assumptions with effective dates and review them against actual performance.
When planners repeatedly add private buffers, the official model loses credibility. Capture why the buffer is needed and improve the underlying standard. A transparent conservative assumption is more useful than false precision surrounded by unofficial protection.
New products should use deliberately cautious values until enough execution evidence exists. Mature products can earn tighter standards through stable results.
Frequently asked questions
Does finite scheduling guarantee the plan will run?
No. It improves realism by respecting modelled constraints. Execution still depends on current material, equipment, quality and people readiness.
Should the factory always minimise changeovers?
No. Longer campaigns can improve setup efficiency but delay priorities or create inventory. Balance transition cost with customer promise and total flow.
How long should the freeze window be?
Long enough to protect preparation and execution, but short enough to respond to real changes. The appropriate duration depends on product mix, setup and supply stability.
What should happen when a reel is missing?
Expose the affected job and options, confirm the material recovery time, compare alternative sequences and record the authorised decision and customer consequence.
Is machine data essential?
It can improve timeliness, but disciplined operator reporting can support a useful first stage. Shared definitions and reliable events matter more than automation alone.
Make the schedule executable
The most impressive schedule is not the one with the most detailed bars. It is the one the factory can run with minimal surprise and explain when reality forces change.
Connect capacity to readiness, sequence to setup, and execution to the next decision. Then one missing reel becomes a managed exception instead of the start of an invisible chain reaction.