

The Schedule Is Green. Why Is the Line Still Waiting?
A production schedule is credible only when demand, materials, engineering, resources and shop-floor reality agree on what can start next.
The short answer
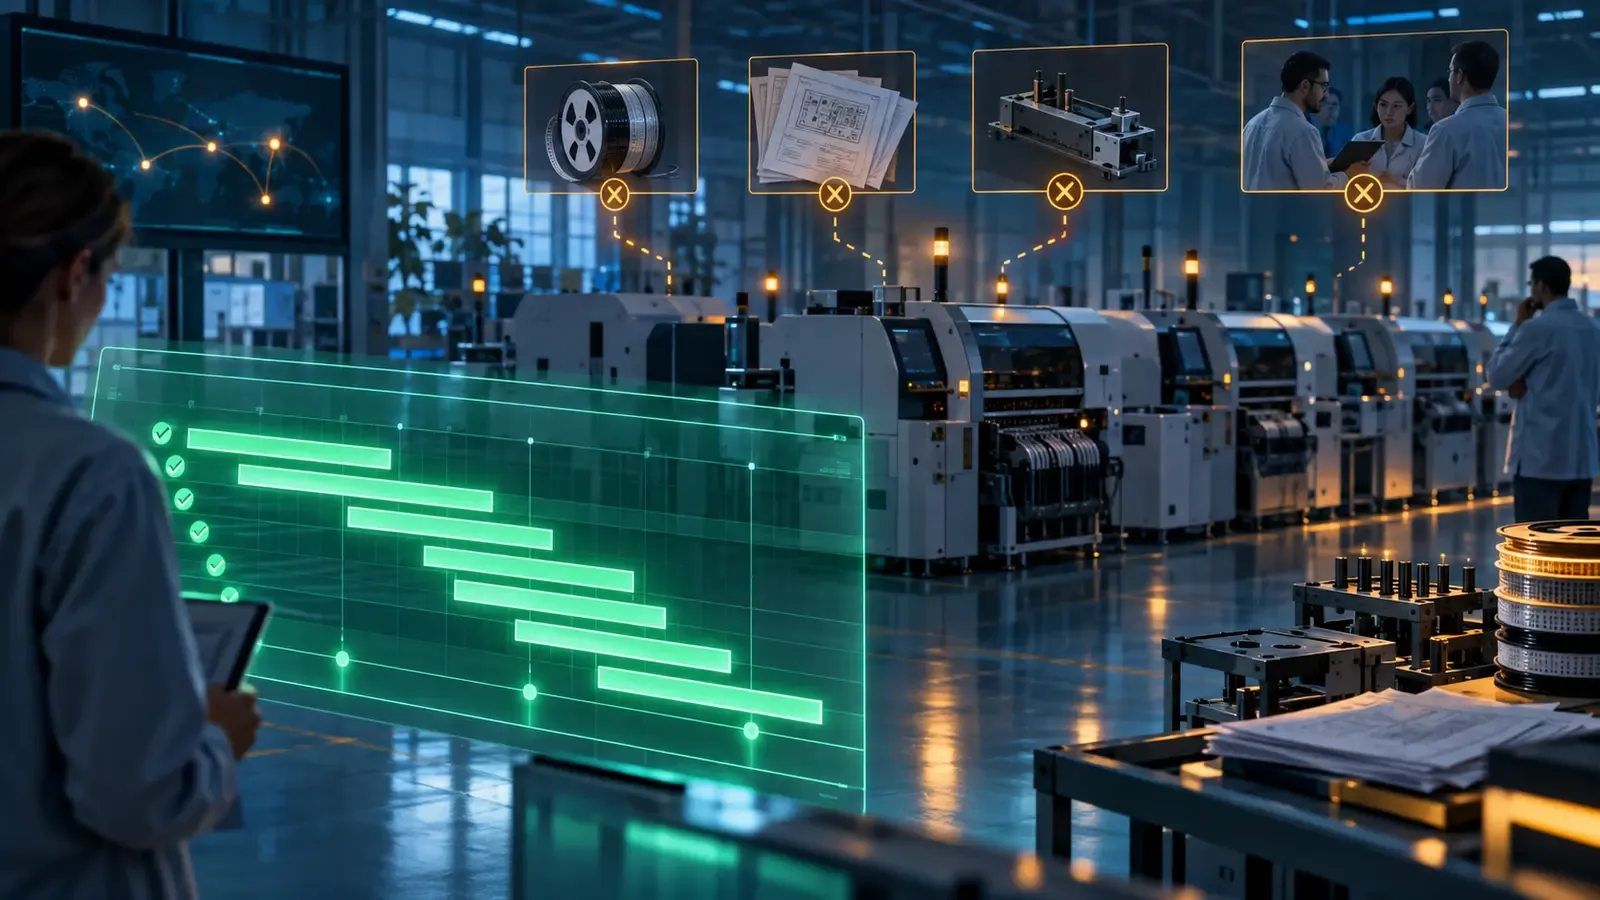
A green production schedule does not prove that a job can start. It only proves that one planning layer has assigned demand to a date or resource. An executable electronics manufacturing plan must also confirm the correct engineering revision, usable material, approved alternates, line configuration, tooling, people, test programmes, quality status and current shop-floor conditions. When those signals live in separate spreadsheets and systems, the schedule can remain green while the line waits.
The practical answer is to manage readiness as a connected operational state. ERP should hold demand, material, engineering and commercial commitments; MES should return actual execution events; and planners should see exceptions before a job reaches the line. The objective is not a prettier schedule. It is a credible promise about what the factory can do next.
A scheduled job is not necessarily a ready job
Electronics factories are full of plans that are technically correct but operationally impossible. A work order fits into an eight-hour shift. The machine appears free. Standard hours suggest that the quantity can be completed. MRP shows no shortage at total inventory level. On a planning board, every condition looks acceptable.
At the line, however, the first component reel is still under incoming inspection. The approved substitute applies to another customer programme. The latest engineering change has not reached the machine programme. A fixture is being repaired. The operator certification has expired. A previous job is running long because inspection found an intermittent defect. None of these facts necessarily changes the coloured bar on a disconnected schedule.
This is the central problem in electronics production planning and control: the plan is an agreement among many types of readiness, not merely an allocation of hours.
Five promises inside every production date
Every scheduled start quietly contains at least five promises.
The demand promise
The job must represent the current customer requirement: the right product, quantity, delivery date, priority and commercial status. If an order has changed but production still works from the earlier release, a schedule may execute efficiently and still produce the wrong commitment.
The engineering promise
The factory must build the correct revision with the correct bill of materials, routing, work instructions, machine programmes and inspection criteria. Revision effectivity matters because a new BOM is not automatically appropriate for every open job or every unit already in WIP.
The material promise
Required components must be physically available, usable, allocated and accessible at the time of need. A quantity shown on hand may be reserved, quarantined, at another site, tied to an older revision or arriving after the planned start. That is why MRP availability can still produce a short kit.
The capacity promise
Capacity includes more than machine hours. It includes qualified operators, feeders, stencils, fixtures, test stations, maintenance condition, changeover time and downstream space. An SMT line that is open on the calendar may not be ready for the assigned product, as explored in why a free SMT line may still be unable to start.
The execution promise
The factory must be able to capture what actually happened and compare it with what was planned. Without timely start, completion, hold, scrap, rework and consumption signals, tomorrow’s schedule is built on yesterday’s assumptions.
Why conventional planning boards become falsely reassuring
Many planning processes compress complexity into one status: planned, released or green. That simplification is useful for presentation but dangerous for decision-making. It treats missing evidence as if it were positive evidence.
For example, “no material shortage” may mean that the last MRP run found enough aggregate stock. It does not necessarily mean that the correct revision is kitted at the correct line. “Engineering released” may mean that a document was approved. It does not prove that all affected programmes and instructions were updated. “Machine available” may mean that no order occupies the time slot. It does not confirm that the feeder setup, fixture and first-article resources are ready.
A credible system separates these signals. It shows which readiness checks have passed, which are pending, who owns each exception and when the fact was last verified. The planner can then distinguish a real green job from a job that is green because nobody has reported the obstacle yet.
Planning should expose constraints before dispatch
The best time to discover a start blocker is not when operators are standing beside an idle line. Readiness review should happen far enough ahead for someone to act.
A rolling horizon works well. Longer-range planning can focus on capacity, supplier commitments and major engineering risk. Near-term planning should become progressively stricter: material allocation, revision effectivity, tooling, programmes, labour and quality disposition must be confirmed. The frozen dispatch window should contain only jobs that meet an agreed release rule, or jobs with an explicitly accepted exception.
This does not mean refusing to schedule anything uncertain. Manufacturing always contains uncertainty. It means making uncertainty visible and owned. A planner may deliberately reserve capacity for a job awaiting one incoming reel, but the schedule should show the dependency, expected resolution time and fallback sequence.
One digital thread from engineering to execution
The Mars platform is positioned around integrated ERP, MES and shop-floor intelligence for electronics manufacturing. That architecture matters because each planning decision depends on data created elsewhere.
An engineering change can alter component demand and machine setup. A supplier delay can change the feasible sequence. A quality hold can reduce usable stock. A shop-floor loss can consume capacity. A customer priority change can alter the commercial consequence of lateness. When these events update one connected model, the plan can respond. When they arrive through meetings and spreadsheets, planners spend their time reconstructing reality.
The electronics industry’s digital-manufacturing direction also emphasises exchange between executable processes and host systems. The value is not connectivity for its own sake. It is the ability to turn equipment, material and production events into decisions while those decisions can still influence delivery.
Readiness must be specific, not generic
A common planning mistake is to approve something globally when the approval is contextual.
An alternate component may be technically acceptable for one product but not another. It may be approved for one customer programme, factory, date range or revision. The same principle applies to test programmes, work instructions, tooling and processes. A simple “approved” flag removes the context that made the approval valid.
The article The Alternate Part Is Approved. But for Which Customer? explains why alternate-component control must preserve product, customer, revision, site and effectivity. The schedule should evaluate those relationships against the actual job rather than assume that any available substitute can close a shortage.
Engineering change is also a planning event
An ECN is often managed as a document workflow: request, review and approval. The operational consequences begin after approval. Open purchase orders, stock, kits, WIP, machine programmes, inspection plans and customer deliveries may all require different actions.
If the BOM changes after kitting, the factory needs a controlled answer to a deceptively simple question: which version should this job build? The answer depends on effectivity and disposition, not the timestamp of the latest document. The BOM Changed After Kitting. Which Version Builds? follows that decision across engineering and production.
Planning must therefore treat engineering change as a constraint update. A job should not remain ready if one of its defining records has changed without downstream confirmation.
Activity is not the same as flow
Another false green signal appears after production begins. WIP may be scanned at several stations and still spend most of its life waiting. High transaction volume can create the appearance of movement while queues grow between processes.
Useful WIP visibility measures elapsed time, queue age and hold reason, not only the last completed operation. It should reveal which units are waiting for material, engineering, test, quality disposition, maintenance or downstream capacity. WIP Is Moving. Why Is Lead Time Getting Longer? examines how factories can look busy while customer lead time deteriorates.
This information must return to planning. If a bottleneck is accumulating two shifts of queue, continuing to release upstream work may raise utilization locally but make the overall promise less credible.
The digital thread must cross factory boundaries
Many EMS routes include external processes. Boards may leave the main site for coating, specialist testing, finishing or another subcontract operation. A purchase order and shipment record can control the commercial movement, but the product’s manufacturing identity also needs to travel.
The receiving party needs the correct revision, serial or lot identity, process requirement and inspection criteria. The sending factory needs evidence of what occurred, which material or equipment was used, what exceptions arose and which units returned. Otherwise, planning sees “at subcontractor” as a single opaque status.
The Board Left for Subcontracting. Did Its History Go Too? shows how an external process can remain part of a continuous product genealogy rather than become a gap in it.
Recovering the schedule requires business priorities
No plan survives unchanged. A machine fails, material arrives late, yield drops or a customer brings a requirement forward. Recovery is not simply the act of rescheduling every delayed order to the earliest open slot.
Every recovery choice changes something else. Expediting one job may break a family sequence, increase changeover, consume a scarce component or delay a higher-consequence order. Overtime may recover shipment date but raise cost and quality risk. Moving production to another site may create transport, tooling and approval constraints.
The recovery process therefore needs explicit priority rules. Customer commitment, contractual consequence, material shelf life, downstream dependency, revenue, margin, strategic relationship and technical risk may all matter. The Plan Slipped Today. Which Order Should Recover First? describes a disciplined way to make that trade-off visible.
A practical readiness model
Manufacturers do not need to model every possible condition on day one. Start with the recurring reasons jobs fail to begin or finish as planned.
For each near-term job, track a small set of readiness dimensions:
- demand and customer release;
- engineering revision and effectivity;
- material availability, allocation and quality status;
- tooling, programme and equipment readiness;
- labour and certification;
- first-article or quality requirements;
- downstream capacity and external-process commitments.
Each exception should have an owner, expected resolution time and defined consequence. The system should refresh readiness when a relevant event changes, not only during a daily meeting.
Once those signals are reliable, planners can create dispatch rules. A fully ready job may enter the frozen schedule. A conditionally ready job may require approval. A blocked job remains visible but does not consume executable capacity. This turns the schedule from a picture of intention into a controlled queue of feasible work.
What management should measure
Traditional adherence asks whether a job started or finished on the planned date. That remains useful, but it describes the outcome after the opportunity to prevent delay has passed.
Add leading measures:
- percentage of jobs fully ready at the freeze point;
- number and age of unresolved start blockers;
- schedule changes caused by material, engineering, equipment and quality;
- time between an exception event and planning acknowledgement;
- WIP queue age at constrained operations;
- percentage of recovery decisions made with documented priority logic;
- plan stability inside the frozen horizon.
These measures reveal whether the planning process is becoming more credible. They also prevent teams from hiding structural problems by continually moving dates.
The management question that changes behaviour
Instead of asking, “Is the schedule complete?”, ask, “What evidence says each near-term job can start and flow?”
That question changes the conversation. Materials cannot answer only with total stock. Engineering cannot answer only with document approval. Production cannot answer only with machine availability. Each function must connect its evidence to the specific job and time window.
This is the operational advantage of a unified ERP and MES model. The factory does not eliminate uncertainty, but it stops treating disconnected assumptions as confirmed readiness. The schedule becomes a living control system that links customer promise, product definition, material truth and execution reality.
Frequently asked questions
Why can a production schedule be green when the line is idle?
Because the schedule may confirm only time and machine allocation. Material quality, revision effectivity, programmes, tooling, labour, inspection or a previous job’s overrun may still block the start.
What is the difference between planning and dispatching?
Planning balances demand and resources across a horizon. Dispatching decides which ready job should run next under current conditions. A good system connects both without pretending that a future plan is already executable.
Should blocked jobs be removed from the schedule?
Not necessarily. They should remain visible with a clear blocker, owner and expected resolution, but they should not be counted as executable capacity unless the risk has been explicitly accepted.
How do ERP and MES support the same schedule?
ERP supplies customer demand, BOM, material, procurement, cost and order context. MES supplies actual starts, completions, consumption, holds, downtime and process results. Planning becomes more credible when the two share consistent identifiers and events.
What should an EMS manufacturer improve first?
Identify the most common reasons jobs fail to start, define a small readiness model for those constraints, assign ownership and connect the evidence to each near-term job. Expand only after the first signals are reliable.