The Offcut Is Small. The Margin Leak Is Not.
Paper and board waste becomes commercially meaningful when size, grain, layout, trim and purchasing decisions remain separated from job economics.
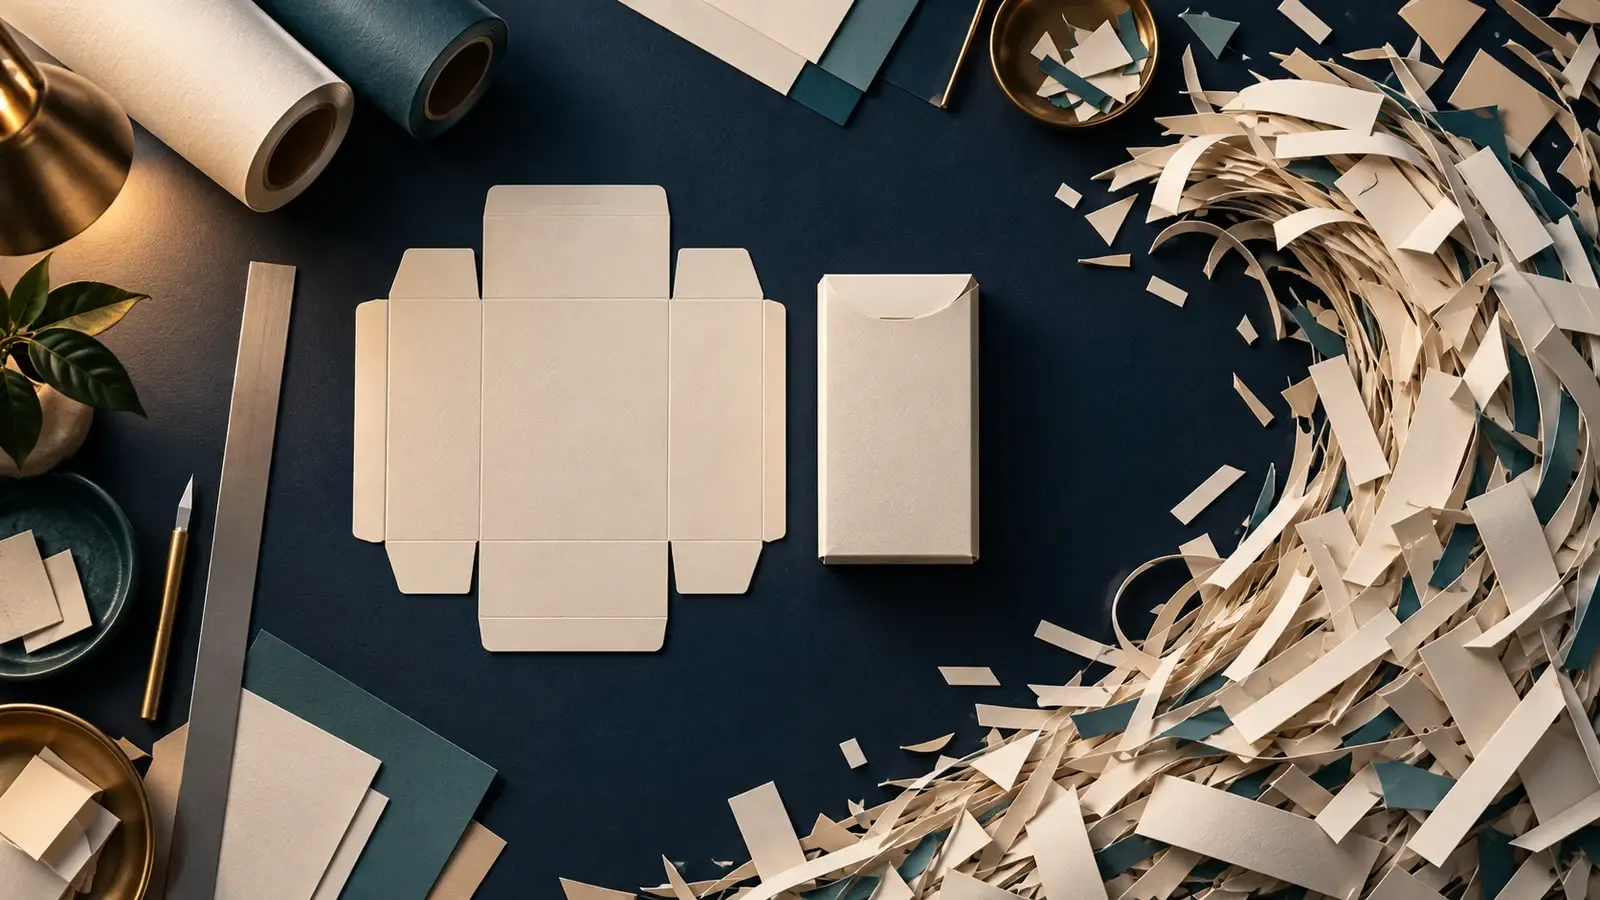
The offcut beside the guillotine looks harmless. It is a narrow strip of clean board, too small for the current carton and too awkward for the next scheduled job.
One strip will not disturb the monthly result. Thousands of strips, trim allowances, wrong-grain substitutions, partial reels and emergency purchases will.
Material loss often enters the factory as a millimetre and leaves the accounts as a margin problem.
The short answer
Paper planning for printing and packaging should connect finished dimensions, imposition, grain direction, trim, sheet or reel availability, process loss, purchasing quantity and actual usage to the same job. Waste becomes manageable when each loss has a reason and commercial consequence—not when all residual material is grouped into one month-end percentage.
The objective is not zero offcut. It is the best feasible conversion of the correct material into accepted product.
Begin with usable specification
Paper and board are described by more than grade and weight. Sheet size, reel width, grain direction, caliper, finish, coating, shade, certification, lot and moisture condition can affect whether stock is usable.
An inventory quantity that ignores these attributes creates false availability. The system may show enough tonnes while the job cannot use the stock without changing imposition, quality or processing.
Define which attributes control allocation for each product. Preserve approved substitutes and the authority required to use them.
Grain belongs in the economic model
Grain direction can affect folding, stiffness, curl, creasing and run behaviour. Rotating a layout may improve geometric yield and damage converting performance.
The planner should see both possibilities: apparent sheet utilization and technically valid utilization. If a grain-compliant layout creates more waste, that is a real job cost—not an inefficiency to hide.
Record the rule at quotation and confirm it at imposition. A later discovery can force a new sheet size, reduced number-up or material purchase.
Millimetres multiply through volume
Trim, bleed, colour bars, gripper and finishing allowances each have a purpose. Overgenerous allowances multiply across every sheet; overly tight allowances increase quality risk.
Standardize by press, process and product family, then review exceptions. If operators routinely add extra trim because downstream registration is unstable, the root issue is not simply paper usage.
Translate the layout into commercial scale. A two-millimetre difference may sound trivial until applied across a high-volume run or a costly specialty substrate.
Plan from available formats, not an ideal catalogue
Estimating may assume an economical standard sheet. Purchasing may find that only another size is available within the lead time. Production then inherits additional trim or a different press route.
Connect availability before commitment where possible. Show the alternatives:
- use stock on hand with a revised layout;
- purchase the ideal size at a later date;
- slit or cut material before production;
- combine jobs to use the format better;
- accept controlled additional waste to protect delivery.
Each option changes cost, capacity or time. The decision should update the job rather than disappear into purchasing notes.
Distinguish planned loss from abnormal loss
Some material does not become saleable product by design: gripper edge, trim, setup sheets, retained samples and expected process spoilage. Other loss comes from defects, wrong versions, damage, poor handling or excess production.
Separate these categories. Planned conversion loss tests the estimate and layout. Abnormal loss tests process control.
A useful material reconciliation can include:
1. quantity issued;
2. planned setup and trim;
3. accepted finished quantity;
4. work in process;
5. recoverable remainder;
6. scrap by reason;
7. unexplained variance.
The units must reconcile. Converting sheets, kilograms and finished units requires controlled conversion factors.
Give remnants a future—or close them honestly
Usable remnants can become value or clutter. A partial reel or stack of offcut may be theoretically reusable but practically unidentifiable.
Record material identity, dimensions, grain, quantity, condition and location. Set a minimum threshold for return to stock. Small remnants below practical use may be recorded as scrap rather than filling racks with false assets.
Review ageing. Material that has remained “reusable” for a year may be tying up space and overstating inventory value.
Imposition and purchasing should share evidence
Prepress optimizes the sheet; purchasing optimizes the order quantity and price. If they work independently, a cheaper bulk purchase may create more leftover stock than the job family can consume.
Share forecast demand, viable formats and actual yield. For repeat products, compare several purchase sizes across expected jobs rather than optimizing one order alone.
The gang-run decision can also improve use, but it should not delay work or create incompatible promises merely to consume a sheet.
Connect waste to the job margin
Monthly waste percentage is useful for a plant trend and weak for diagnosis. The business needs to know which jobs, materials, presses, layouts and causes produced loss.
Assign actual material consumption and recoverable returns to the job. Value scrap by the organization’s accounting policy. Show variance against the estimate.
An integrated solution such as Jupiter ERP supports paper planning, imposition, BOM and job costing within the print workflow. The operational value comes from recording real issue, return and waste events accurately.
Sustainability claims need material evidence
Good yield reduces cost and avoids unnecessary material consumption. But sustainability communication should rest on defined data and responsible claims.
Two Sides describes paper-based packaging as part of a renewable and recyclable material cycle. That broad context does not remove the manufacturer’s need to track its own fibre specification, certified inputs, waste routes and conversion yield.
Avoid turning one improved layout into an unsupported environmental claim. Use traceable measures and explain boundaries.
Review waste where it is created
A monthly number arrives too late for the job. At the press or finishing process, record reason while evidence is fresh: makeready, colour correction, register, damage, die-cut failure, wrong revision, overproduction or trim.
Keep the list short enough to use. Allow notes for unusual causes. Regularly test whether “other” has become a hiding place.
Supervisors should see abnormal accumulation during the run, not only after finance closes the month.
Treat substitute material as a controlled scenario
When the planned stock is unavailable, substitution can protect delivery and quietly change performance. Compare price, usable format, grain, caliper, surface, certification, print behaviour and finishing risk before release.
Record who accepted the substitute and how its expected yield differs. If a cheaper sheet creates fewer ups or more spoilage, purchase-price variance alone gives the wrong signal.
After production, preserve the actual outcome. The next planner can see whether the alternative is genuinely approved and under which conditions it worked.
Follow trim back to design and standards
Some waste cannot be solved on the factory floor. Product dimensions, dielines, standard sheet choices and customer design rules may lock in poor yield.
Use repeated job evidence to start an upstream conversation. A small dimensional adjustment may improve imposition while preserving product function; a family of products might share a more economical format. Any change still needs technical and customer approval, but the opportunity becomes visible.
Balance purchase economics with inventory risk
Volume buying can reduce unit price and create slow-moving remnants. Compare purchase saving with expected consumption, storage, handling, deterioration and cash tied up.
The best order quantity supports a credible family of future jobs, not an abstract price break. Review planned versus actual consumption before repeating the purchase pattern.
Frequently asked questions
Is the layout with the highest number-up always best?
No. Grain, quality, press suitability, finishing, run length and schedule all matter. Optimize accepted finished cost, not geometry alone.
Should every offcut return to inventory?
Only when it is identifiable, usable and economically worth handling. Define practical thresholds and record smaller residuals honestly as waste.
How should paper waste be measured?
Use both physical quantity and financial value, linked to job and reason. Separate planned conversion loss from abnormal loss and reconcile issue, return, output and scrap.
Can sustainable paper eliminate the need for waste control?
No. Responsible sourcing and recyclability matter, but efficient conversion still reduces cost and unnecessary resource use.
Make the small strip visible
The offcut is not evidence that somebody failed. It may be the correct consequence of grain, trim or available stock. The problem begins when its cause and value are unknown.
Inside the shape-shifting print job, material planning translates artwork and product dimensions into physical economics. Make that translation visible, reconcile the result and let every millimetre tell management something useful.